Pilot Production
Manufacture production-intent components for assembly, process and customer validation before scaling.
بيت / خدمات / تصنيع منخفض الحجم
AFTER THE PROTOTYPE. BEFORE THE COMMITMENT.
Move from validated prototypes to production-ready batches.
TOPS Precision provides low-volume manufacturing services for custom metal and plastic components, helping engineering teams move from prototype validation into pilot runs, bridge production and repeat small-batch manufacturing.
We support in-house CNC machining, يموت الصب, تصنيع الصفائح المعدنية وقولبة حقن البلاستيك, with process selection based on your geometry, مادة, تسامح, كمية, tooling budget and future production requirements.
أرسل الرسم الخاص بك, مادة, كمية, tolerance and finish requirements for review.
A production strategy, not a fixed quantity
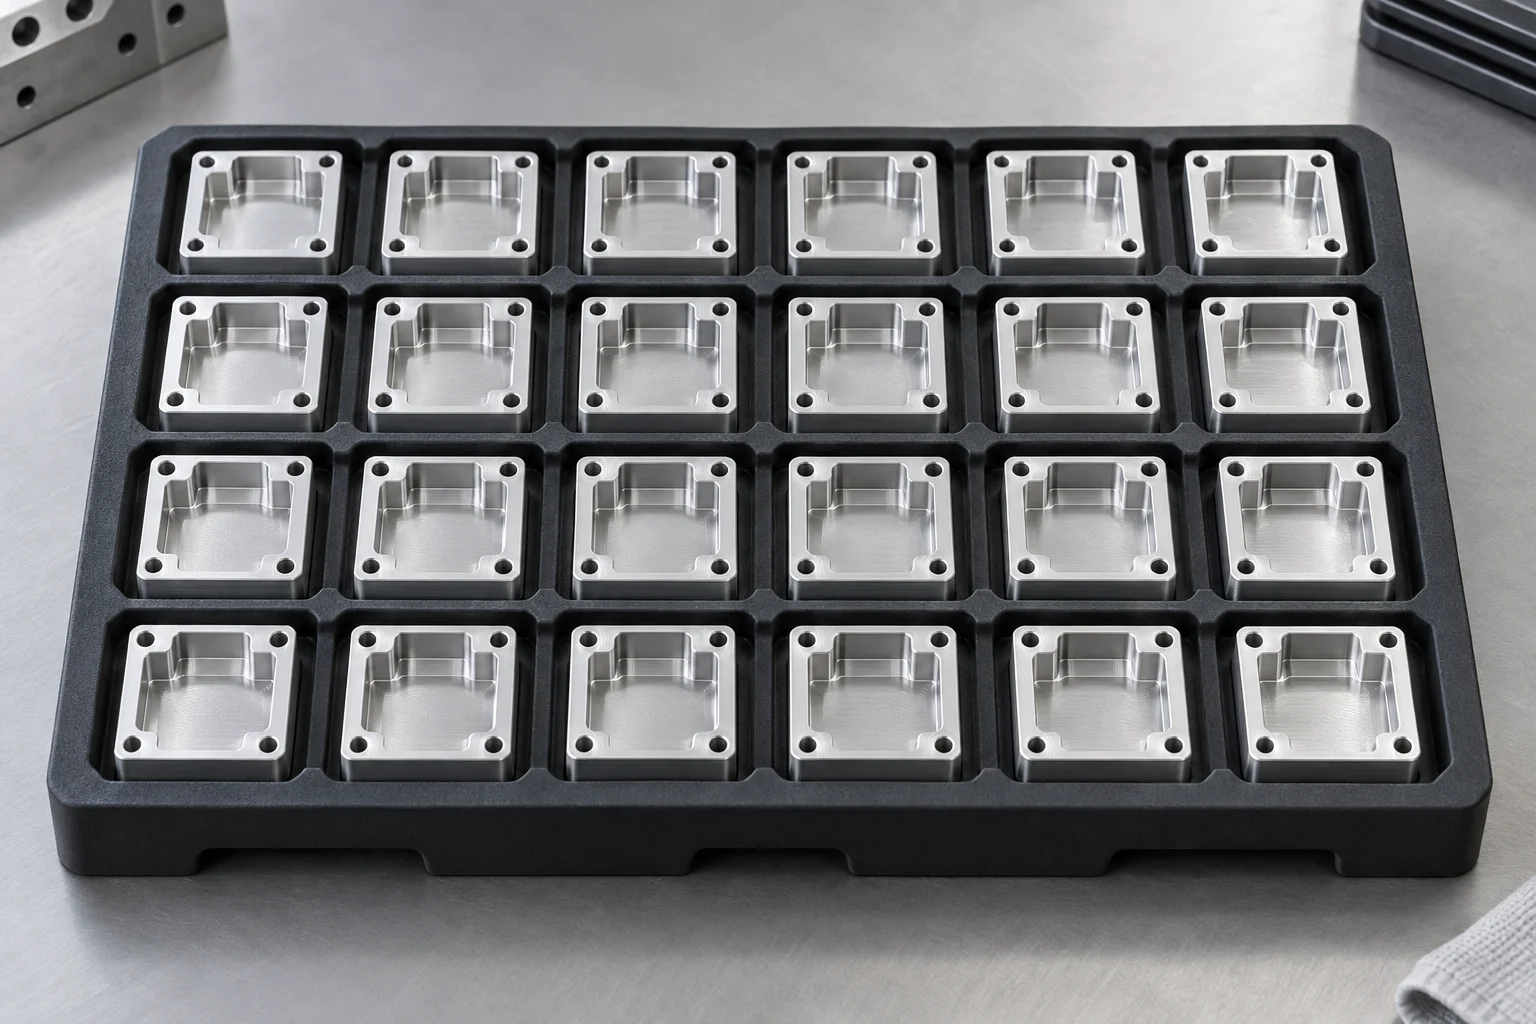
Low-volume manufacturing is the production of functional, production-quality parts in quantities that are higher than prototype demand but lower than traditional mass-production volumes. It is commonly used for pilot builds, إنتاج الجسر, market launches, customized products, replacement parts and repeat small-batch supply.
There is no universal quantity that defines “low volume.” The economical range depends on geometry, عملية التصنيع, الأدوات, مادة, تسامح, order frequency and annual demand.
TOPS Precision manufactures custom metal and plastic parts in Dongguan, الصين. We review the drawing and the production context together to recommend a practical route.
Start with the reason for the batch
Manufacture production-intent components for assembly, process and customer validation before scaling.
Maintain supply while production tooling or a higher-volume process is being prepared.
Release controlled quantities while the forecast and production plan are still developing.
Put functional products into real applications before committing to a large inventory.
Make different configurations where annual demand per variant is limited.
Support recurring low-demand parts without automatically building large stocks.
Four in-house manufacturing routes
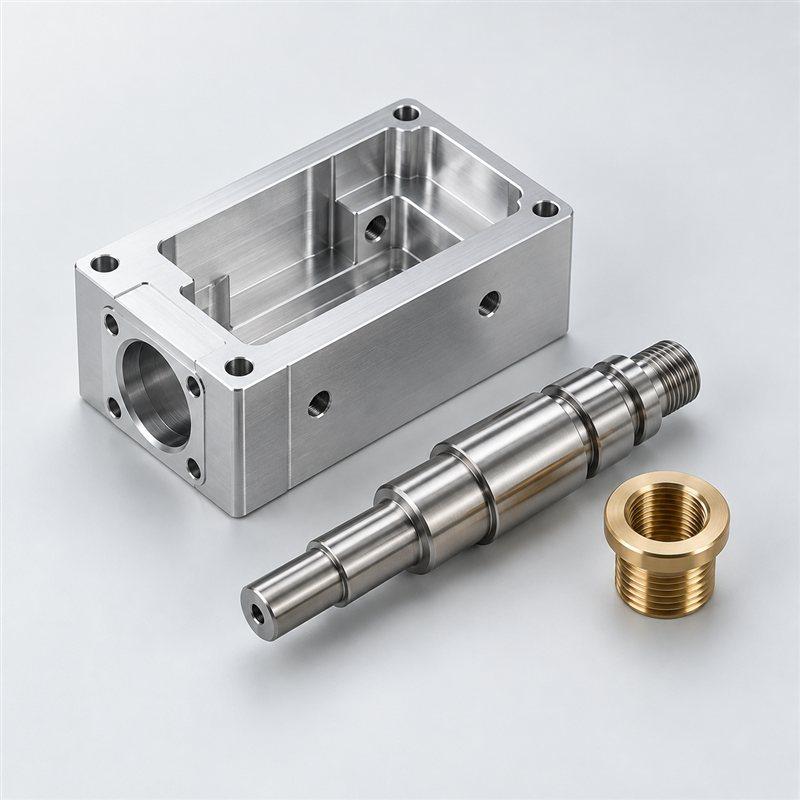
Precision metal and engineering-plastic components, هندسة معقدة, tight tolerances and frequent design changes.
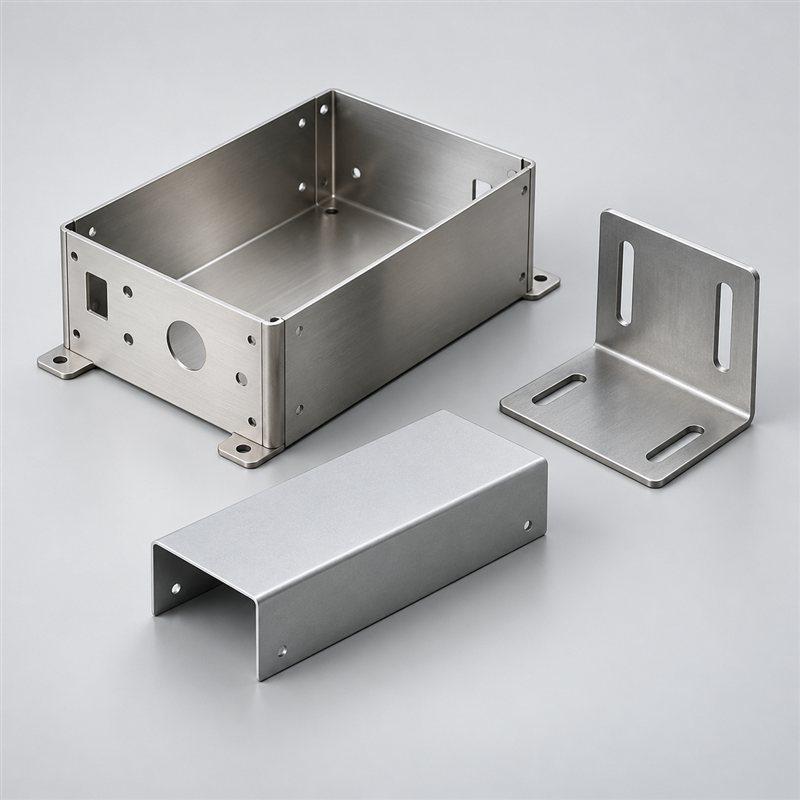
قوسين, حاويات, لوحات, أغطية, chassis and formed components.
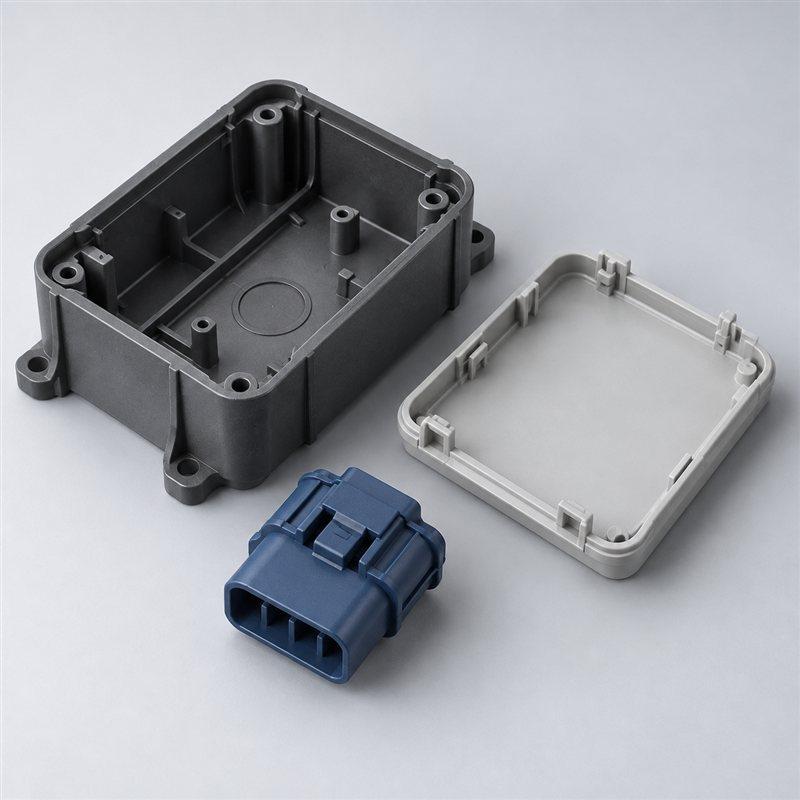
Repeat plastic parts when quantity, geometry and stable design justify tooling.
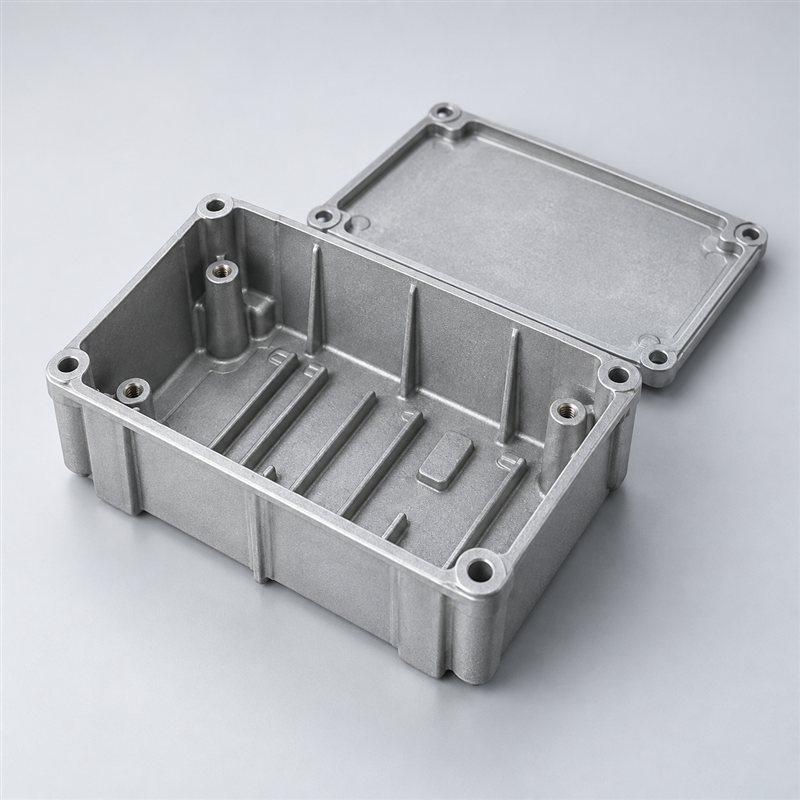
Suitable recurring metal components when tooling economics fit forecast demand.
Die casting is not automatically economical for a small batch. Molding and casting are evaluated against recurring volume, استثمار الأدوات, geometry and design stability.
The route changes as your project matures
These stages describe possible production routes. A project may stay in repeat small batches; it does not have to progress to mass production.
One or a few parts for form, ملائم, function and geometry validation.
Controlled batches for assembly validation, applicable certification tests, process validation and customer approval.
Production-quality supply while demand develops, tooling is prepared or the final route is optimized.
Scheduled batches for specialized equipment, product variants, regional inventory and replacement parts.
Evaluate optimized fixtures, أدوات الإنتاج, casting or molding when stable demand justifies the change.
Quantity is only one input
| متطلبات | Potential manufacturing route | Review before committing |
|---|---|---|
| Tight-tolerance metal part | التصنيع باستخدام الحاسب الآلي | Critical features and inspection method |
| Complex milled housing | 3/4/5-محور CNC الآلات | Tool access, setups and internal radii |
| Cylindrical shaft or bushing | تحول باستخدام الحاسب الآلي | القطر, runout and secondary operations |
| Sheet metal enclosure | القطع بالليزر + الانحناء | سماكة, bend radii and assembly |
| Plastic part before production tooling | التصنيع باستخدام الحاسب الآلي / suitable prototype process | Material equivalence and end use |
| Repeat plastic production | Injection molding if tooling is justified | Design stability and annual releases |
| كرر السكن الألومنيوم | CNC machining or die casting | الهندسة, سبيكة, volume and secondary machining |
| Frequent design revisions | التصنيع باستخدام الحاسب الآلي | Revision control and work in progress |
| No dedicated mold or die desired | CNC machining or sheet metal fabrication | Programming and workholding costs remain |
| Higher recurring volume | Evaluate molding, casting or production tooling | Total cost, forecast certainty and validation |
TOPS reviews annual demand, batch size, هندسة, تسامح, ينهي, مادة, tooling budget and future scalability before recommending the most economical manufacturing route.
Send your drawing and expected quantity. Our team will review the manufacturing route.
Production stock. Flexible geometry.
CNC machining is often an effective low-volume production method because it does not need a dedicated injection mold or casting die. CAD revisions can be implemented relatively quickly, making it suitable for pilot builds, customized products, engineering changes and repeat small-batch orders.
CNC Milling → · CNC Turning → · 4-Axis CNC Machining → · 5-Axis CNC Machining → · EDM Machining →
Grinding and secondary operations are reviewed against the drawing.
View CNC Machining Capabilities →Choose the level of commitment
التصنيع باستخدام الحاسب الآلي, laser cutting and standard fabrication can avoid dedicated molds or dies. Programming and workholding are still required. This route often offers lower initial commitment and easier changes.
Simplified fixtures, prototype or limited-life tooling and manufacturing aids may improve repeatability. ملاءمة, expected life, material and acceptance requirements are evaluated for each project.
قوالب الحقن, die casting dies and dedicated production fixtures can reduce unit cost at sufficient stable volume. Review design maturity, tooling ownership, maintenance and future changes before investment.
Consider tooling investment, engineering-change risk, inventory, batch size, forecast certainty and validation. A route with a higher part price may need less cash or carry less change risk at launch.
Manage launch risk, not just piece price
Avoid committing to dedicated production tooling before geometry and demand are sufficiently stable.
Use a suitable route for functional parts while the longer-term production plan evolves; lead time is quoted per project.
Review and implement revisions before full production tooling is locked, while controlling any existing work in progress.
Release batches closer to actual demand, balancing setup cost and stock requirements.
Assess suitable production-grade materials and functional parts in the intended application.
Validate geometry, حَشد, quality criteria and production assumptions before scaling.
Specify the grade and condition
6061 · 5052 · 7075 · 2024
304 · 316 · 17-4 الرقم الهيدروجيني · 420
1045 · A36 · فولاذ الأدوات · سبائك الفولاذ
النحاس · C360 · C260 · C280
تيتانيوم · إنكونيل · إنفار · كوفار
ABS · POM · PC · Nylon · PEEK · PTFE · PP · PMMA · Torlon
These are material options across suitable processes, not grades interchangeable between machining, sheet fabrication, molding and casting. على سبيل المثال, 5052 suits sheet applications while casting requires a casting alloy. التوفر, condition and process suitability are confirmed at quotation.
عرض جميع المواد →Production intent includes the final surface
Specify alloy, لون, سماكة, masked features and appearance.
Agree coating thickness, wear requirements and dimensional allowance.
Define color, لمعان, سماكة, masking and adhesion requirements.
Specify stainless grade, process and acceptance tests; appearance alone cannot verify passivation.
Agree material, حالة السطح, dimensional allowance and acceptance.
Define coating metal, سماكة, underlayers and any applicable embrittlement controls.
Specify surface roughness, cosmetic criteria and areas to preserve.
تحديد المواد, حالة, hardness and distortion allowance; appearance cannot prove hardness.
Where practical, low-volume production should use the specified finish, inspection criteria and appearance controls required for the intended end-use part. Confirm finishing responsibilities, final-condition measurement and any outside processing in the quotation.
Explore Surface Finishing →A small batch still needs repeatability

CMM · Optical measurement · Micrometers · Calipers · Gauges · XRF where applicable
TOPS reviews critical dimensions, التسامح, material requirements and inspection methods before production so the approved process can be repeated across subsequent orders.
Confirm revision, الأبعاد الحرجة, جي دي&T and acceptance requirements.
Verify grade and condition using the agreed evidence and applicable checks.
Measure initial parts against the agreed plan before release where required.
Check designated features and process checkpoints during manufacture.
Use agreed sampling or 100% checks where specified; do not assume every feature is checked on every part.
Review dimensions, ينهي, identification and packaging before release.
Provide the reports and certificates included in the order.
ايزو 9001:2015 supports quality management. Specify FAI, تقارير الأبعاد, شهادات المواد, RoHS documentation and CoC during quotation. XRF is an applicable alloy-screening method; it does not replace every material test or certificate.
Review Quality & Inspection →An approval gate before the next release
Manufacture initial samples to the approved drawing.
Verify agreed critical dimensions and surface finish.
Resolve deviations and obtain approval where required before continuing.
Manufacture the controlled quantity to the released requirements.
Verify the agreed characteristics and delivery condition.
Confirm revision and reuse approved requirements where applicable.
First article approval, pilot quantity, inspection deliverables and any hold points must be agreed. An approved first part does not remove the need for batch inspection or change control.
Where a controlled batch matters
Custom frames, المفاصل, actuator components, fixtures and equipment parts.
Explore Robotics & Automation →Development components, test parts, المساكن, fixtures and specialty vehicle components.
Explore Automotive & EV →المكونات الميكانيكية, المساكن, fixtures and instrument parts where applicable. Customer-defined regulatory and validation requirements remain part of the review.
Explore Medical Equipment →مكونات الآلة, قطع الغيار, custom equipment and limited-production assemblies.
Explore Industrial Machinery →العلب, heatsinks, brackets and other mechanical components.
Explore Electronics →Mechanical components for energy storage, power equipment and specialized installations.
Explore industries →For flight-related requirements, review aerospace machining applications →. Industry references describe component applications and do not imply specialist regulatory certification.
Match the batch to its job
Define the use, test conditions and acceptance plan for the batch. Certification units must meet the relevant customer and testing-body requirements; manufacturing the parts alone does not certify the product.
Compare total cost and uncertainty
| عامل | Low-volume manufacturing | الإنتاج بكثافة الإنتاج بكميات ضخمة |
|---|---|---|
| Initial investment | Often lower without dedicated tooling | Often higher with production tooling |
| الأدوات | Low or moderate, depending on route | Can be significant |
| مرونة التصميم | Usually higher before dedicated tooling | Changes can be harder after tooling release |
| Unit cost | Often higher because setup is spread across fewer parts | May be lower when volume offsets tooling and setup |
| Inventory risk | Smaller releases can limit stock exposure | Larger runs can increase stock exposure |
| Lead time to start | Often shorter for mold-free routes | Tooling and validation may extend launch |
| Engineering changes | Often easier; stock and setup still matter | May need tool modifications and revalidation |
| Best fit | Pilot, كوبري, variants and specialized demand | Stable design and sustained higher demand |
These are typical tendencies, not universal price or lead-time promises. Compare an actual quotation, expected releases, inventory costs and the probability of design changes.
Give each build a distinct purpose
| عامل | النماذج الأولية السريعة | Low-volume manufacturing |
|---|---|---|
| Goal | Validate design, ملاءمة والوظيفة | Supply pilot, bridge or repeat production batches |
| كمية | One or a few test parts, as needed | Controlled batch releases |
| عملية | Chosen for validation; may differ from final production | Chosen for production intent and economical repeatability |
| تقتيش | Check the features needed for validation | Check agreed first-article and batch acceptance criteria |
| التكرار | May already be critical to the test | Controlled consistency across the batch and future releases |
| End use | Testing and development; some prototypes are functional | Testing and appropriate end-use supply |
Explore rapid prototyping → for early design-validation parts. For technical process detail, view precision manufacturing capabilities →. For ongoing OEM program management, explore contract manufacturing →.
Specific support for engineering buyers
Four in-house routes let process selection evolve with geometry, مادة, design maturity and demand.
Review manufacturability, مادة, tolerance risk and cost drivers before production.
Evaluate quantities against process, هندسة, tooling and commercial requirements instead of promising a universal MOQ.
Select dimensional verification around the critical features and agreed acceptance criteria.
Carry approved technical requirements into later builds within the same supplier relationship.
Coordinate quotation, إنتاج, packaging and shipping arrangements with overseas engineering and sourcing teams.
Requirements → review → release
Send 3D CAD, 2رسومات د, part revisions, مادة, batch quantity, annual demand, التسامح, finish and quality requirements.
Review manufacturability, tolerance risk, مادة, عملية, tooling and cost drivers.
Agree price, manufacturing route, الأدوات, inspection scope and expected lead time.
Produce and inspect the initial parts where appropriate; follow the agreed approval hold points.
Manufacture the approved batch to the released drawing and requirements.
Complete agreed final inspection, تعريف, protective packaging and shipment.
A quick production-strategy check
Select Yes or No for each question. This guide identifies reasons to discuss a small-batch route; it does not replace a drawing or cost review.
Answer the questions to see which production considerations apply.
Discuss Your Production Strategy ↗Direct answers for sourcing teams
Low-volume manufacturing produces functional, production-quality parts in small batches for pilot builds, bridge supply, product launches, custom variants and repeat low-demand orders. It connects prototype validation with an appropriate production route. The manufacturing process and acceptance criteria should fit the intended use rather than treating the batch as a collection of appearance models.
There is no universal quantity that defines low-volume manufacturing. The economical range depends on geometry, عملية, مادة, الأدوات, تسامح, batch size, order frequency and annual demand. Send both the quantity per batch and the annual forecast. TOPS reviews the practical production route and quotation quantities for each part; this page does not promise a universal MOQ.
Prototyping primarily validates a design, while low-volume manufacturing supplies controlled batches for pilot, bridge or end-use production. Both can use production-grade materials and close inspection. Low-volume work places additional emphasis on repeatability, revision control, batch acceptance and repeat supply. A prototype process or material may need to change before it represents the intended production part.
Bridge production supplies parts during the transition to a planned production process or higher-volume tooling. على سبيل المثال, CNC-machined parts may support a launch while injection tooling is prepared. The temporary route still needs agreed material, وظيفة, tolerance and inspection requirements. Differences between machined, molded and cast parts must be reviewed before substitution.
Pilot production is a controlled initial batch used to assess the planned part, assembly and manufacturing process before wider release. It can support assembly trials, customer approval and certification testing where applicable. The customer defines testing and regulatory requirements. Pilot acceptance should identify drawing revisions, الميزات الحاسمة, inspection records and any corrective actions before the next batch.
CNC machining and sheet metal fabrication are often practical starting points because they can avoid dedicated molds or dies. Injection molding and die casting can be suitable when geometry, repeat demand and tooling economics justify the investment. مادة, التسامح, ينهي, design-change risk and total project cost determine the route; quantity alone does not select the process.
نعم. CNC machining is suitable for many low-volume metal and engineering-plastic components because it uses production-grade stock without a dedicated injection mold or casting die. برمجة, workholding and inspection still have setup costs. طحن, تحول, التصنيع باستخدام الحاسب الآلي متعدد المحاور, موسيقى الرقص الإلكترونية, grinding and secondary operations can be combined around the drawing and batch requirements.
Consider switching when stable design and recurring demand make tooling economically and technically worthwhile. Compare tooling cost, unit cost, expected releases, التغييرات الهندسية, inventory and lead time. Also review draft, سمك الجدار, انكماش, material properties and secondary machining. A CNC prototype does not automatically validate the geometry or properties of a molded or cast version.
نعم. TOPS supports repeat small-batch production against approved drawings and agreed acceptance requirements. Identify the part number, revision, quantity per release and expected annual demand. Changes in material, تصميم, tooling or inspection should be reviewed before the next release. Schedules, stock commitments and documentation are established in the quotation or order.
TOPS can review CNC tolerances down to ±0.005 mm on suitable features. This is not a blanket tolerance for all materials, dimensions or manufacturing processes. Achievability depends on geometry, مقاس, material stability, يثبت, finishing and measurement. Identify critical dimensions and GD&T on the drawing so acceptance criteria can be confirmed before production.
نعم. Low-volume parts can use production-grade metals, engineering plastics and specified surface finishes where the selected process is suitable. State the exact grade, حالة, طلاء, سماكة, masked areas and appearance criteria. Molded and machined polymers or cast and wrought alloys can behave differently, so process substitutions need an engineering review.
Provide 3D CAD and a 2D drawing, part number and revision, مادة, batch quantity, annual forecast, التحمل الحرجة, ينهي, inspection documents, target delivery date and destination. Tell us whether the project is a pilot build, bridge supply or repeat batch. Note any NDA or restricted-file requirements before sharing confidential information.
Ready to start a low-volume production run?
Upload your CAD files and tell us your material, batch quantity, annual demand, تسامح, finish and delivery requirements.
Need to send multiple parts or larger files? Contact info@tops-precision.com for a suitable transfer option.
Quotation confirms feasibility, عملية, الأدوات, scope and lead time. No universal one-day delivery or minimum quantity is implied.