Injection molding color approval requires an agreed reference, comparison conditions, and release criteria for the finished part. A color code alone leaves important decisions unresolved. Define the resin, سطح, إضاءة, measurement method, and approval authority before production. Connect every accepted sample to its revision and manufacturing records.
Choose The Reference That Controls Production
Your color approval should identify the physical or digital reference that governs acceptance and its revision.
A brand color code communicates your starting target. It does not document every condition needed to judge a molded component.
Identify whether your controlling reference is a color plaque, an approved molded part, or an agreed digital standard. Define which reference prevails if they disagree.
Label retained physical references with the part, مراجعة, approval date, and owner. Protect them against contamination, ضرر, and uncontrolled replacement.
A polished plaque and a textured housing represent different surfaces. Approve their relationship before using one to release the other.
For assemblies, include the adjoining components that must look consistent. A separately acceptable cover can still look different beside its mating bezel.
Define Color Lighting And Viewing Conditions
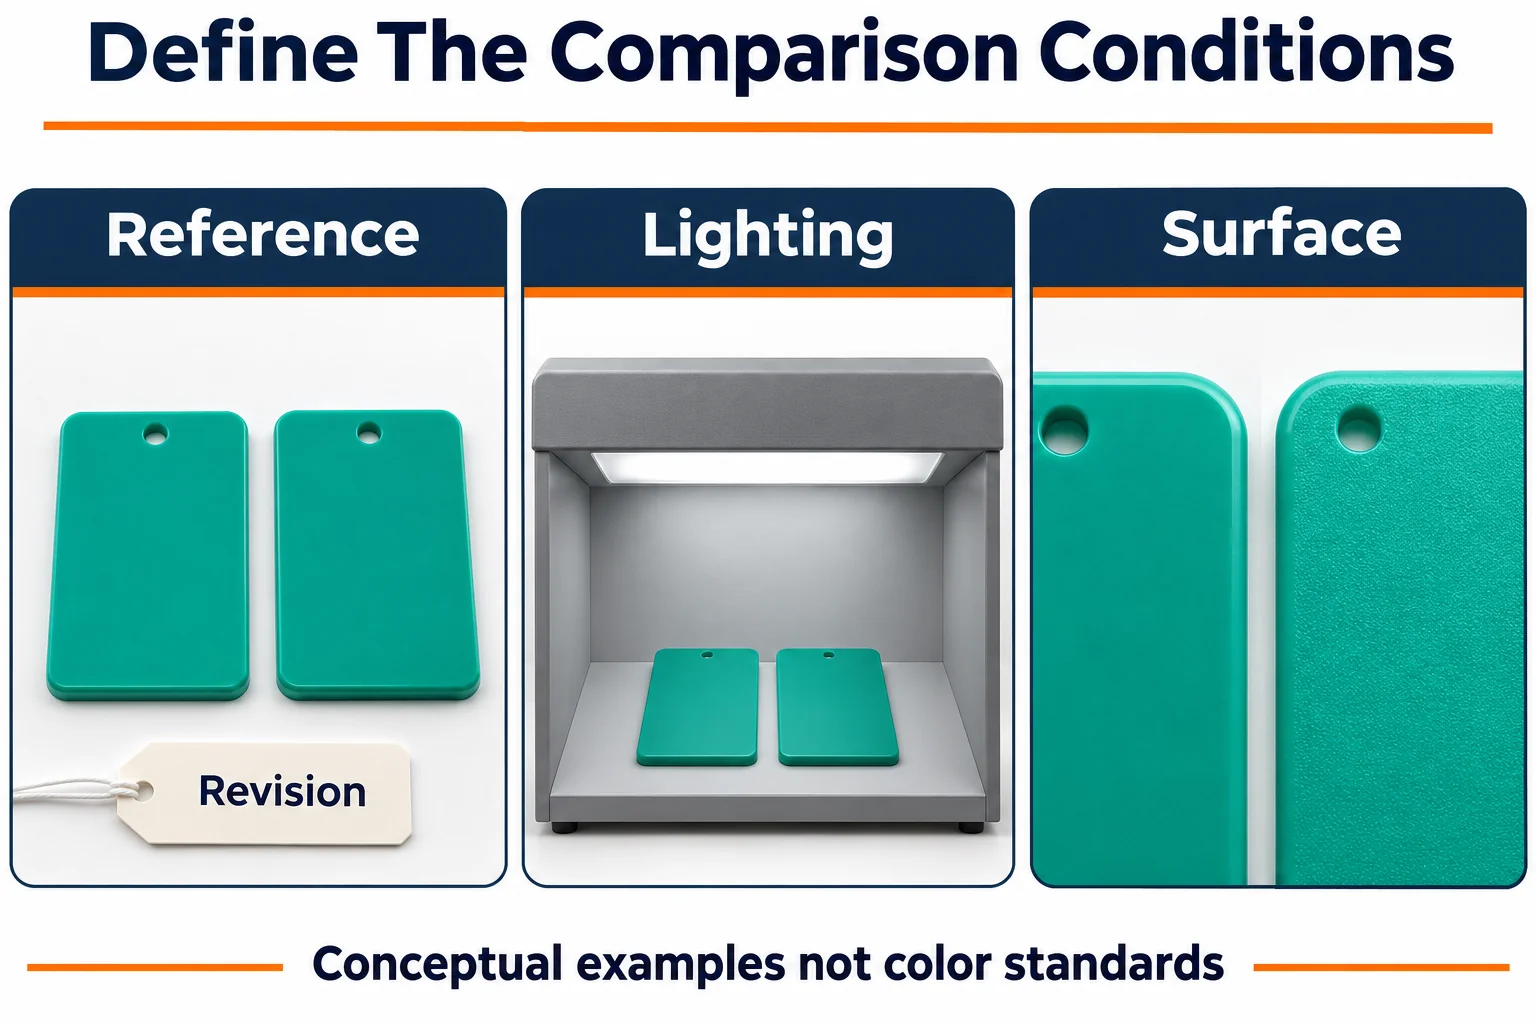
Your visual approval method should fix the light sources, viewing arrangement, and surfaces being compared.
Metamerism means samples can match under one light source and differ under another. X-Rite explains this in its controlled lighting guidance.
Choose evaluation lighting that represents your specified application. Agree any additional light sources needed to assess the match.
Compare the reference and sample together, using a controlled background and consistent orientation. Specify the viewing distance and any relevant angles.
Avoid deciding acceptance from a phone photograph or an uncontrolled office desk. Images can support communication, but they cannot reproduce your approved viewing conditions.
If visual and instrumental results conflict, use an agreed escalation route. Identify who can approve, reject, or authorize a deviation.
Separate Color From Gloss And Texture
You should specify gloss and texture separately when they influence the required appearance of your molded part.
Konica Minolta describes how mold surface texture affects molded appearance. Color agreement alone does not define the entire surface requirement.
Identify visible zones and the intended surface condition in each zone. Include the tool texture reference or approved surface sample where applicable.
Review color in the final specified surface condition. An earlier smooth sample should not silently become the standard for a textured production surface.
Treat gloss bands, الشرائط, and local discoloration as separate acceptance questions. A single average color reading can miss a localized appearance problem.
For defect terminology, انظر لدينا injection molding cosmetic defects guide. Define your project limits rather than relying on a generic defect list.
Agree The Instrumental Measurement Method
Your color tolerance needs a defined measurement method before a numerical result can support release.
Konica Minolta’s measurement standardization guidance explains why instruments and comparison settings must be coordinated across locations.
Specify the color-difference formula and its acceptance limits. Also identify the illuminant, observer, instrument geometry, and specular settings where applicable.
Different formulas and measurement settings can produce different results. Do not treat every value labeled Delta E as interchangeable.
Confirm that the measurement area suits the instrument aperture. Agree the location, توجيه, number of readings, and any approved fixture.
For translucent parts, control backing and thickness where relevant. An opaque plaque may not represent the appearance of a thinner translucent wall.
X-Rite lists backing, سماكة, and aperture among the variables affecting color measurements.
Require a demonstration on representative parts if curvature, نَسِيج, or limited access makes positioning difficult. Approve any surrogate plaque method explicitly.
| بند الموافقة | معلومات للموافقة |
|---|---|
| Controlling reference | Sample or digital standard, مراجعة, ملكية, and replacement rules |
| Visual comparison | Light sources, background, distance, توجيه, and visible zones |
| Instrumental method | Formula, حدود, هندسة, aperture, إعدادات, and measurement locations |
| Surface requirement | نَسِيج, gloss criteria, local defects, وحالة الفحص النهائي |
| Disagreement route | Review evidence, decision authority, and written deviation process |
Control Sample Condition And Production Changes
Your approval plan should compare samples under agreed conditions and identify changes that require renewed review.
BYK’s injection molding quality guide discusses processing effects on color and gloss. It also explains why sample temperature matters for comparable results.
Define when parts are inspected after molding and how their condition is controlled. Do not compare warm production samples with cooler references without an agreed method.
Record the resin grade, colorant identification, and relevant material lots. Define permitted recycled or reprocessed content separately.
Identify changes requiring notification or reapproval. Examples include resin substitution, colorant changes, tool texture work, and manufacturing site transfers.
Agree how these changes affect existing approvals before implementation. Retaining the same color code does not automatically preserve the accepted appearance.
Link Color Acceptance To Lot Release
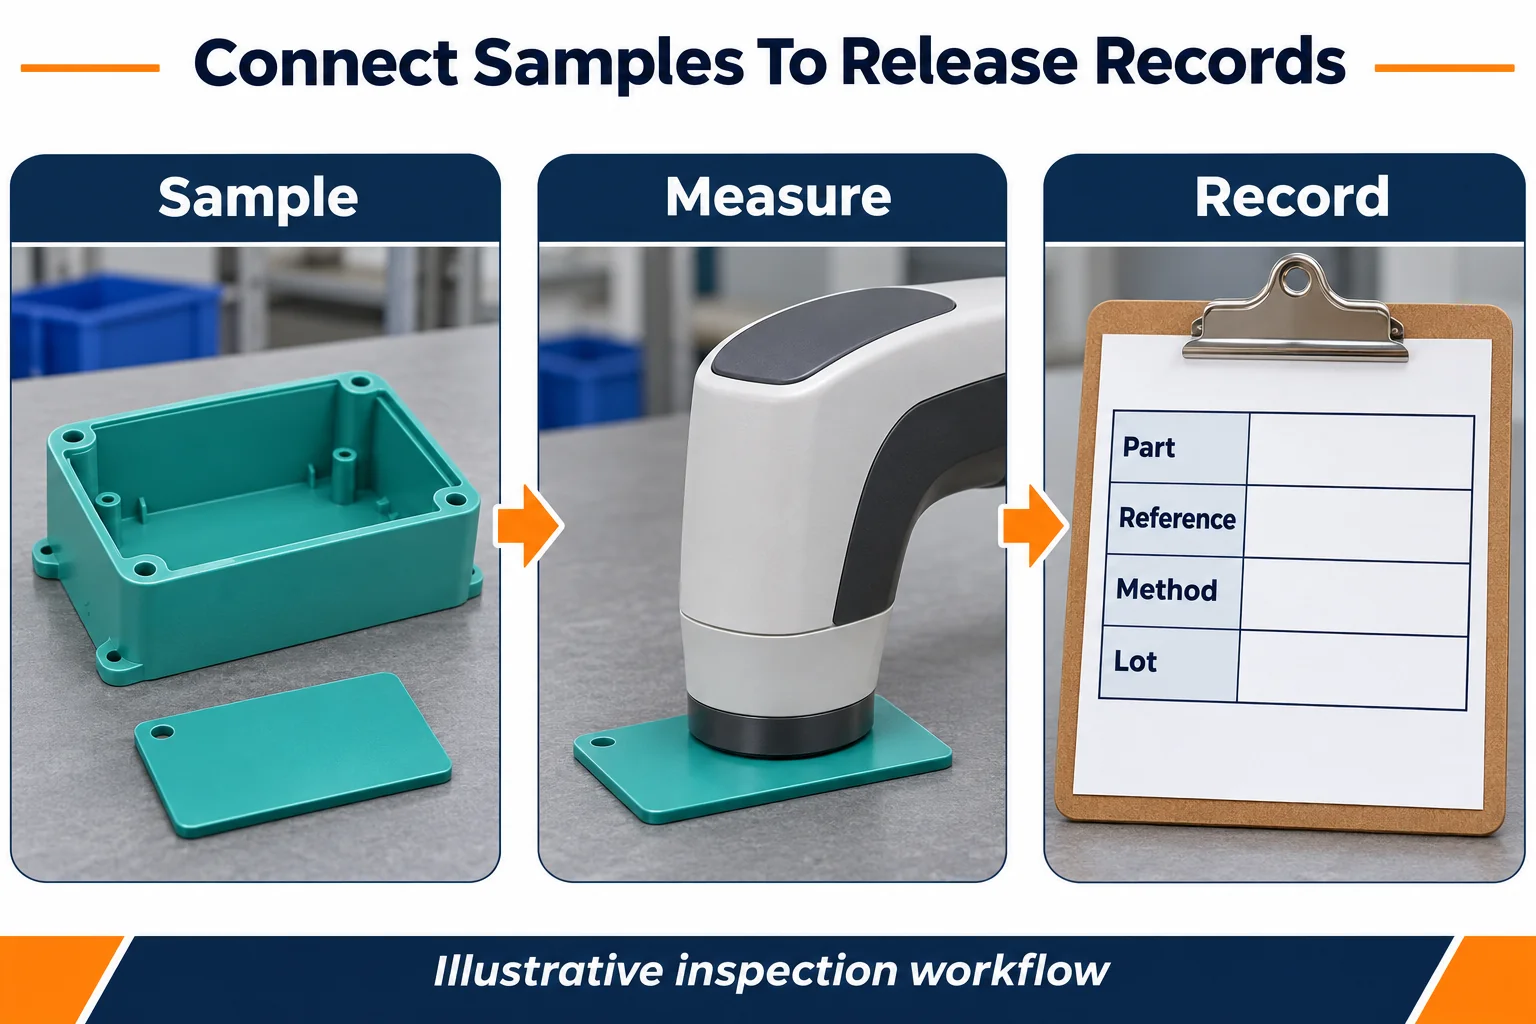
Your release records should connect the evaluated samples to the production lot and approved acceptance method.
Define sampling coverage across cavities and production periods according to your quality plan. Avoid approving an entire program from one unidentified sample.
Record reference revision, تحديد العينة, شروط التفتيش, نتائج, والتصرف. Preserve the decision when an appearance deviation is accepted.
Keep containment and corrective action separate from the release decision. A suspected cause does not establish whether affected parts meet requirements.
| شهادة | غاية |
|---|---|
| Approved reference record | Identifies the target and controlling revision |
| Representative sample approval | Establishes the accepted part and surface condition |
| Inspection method record | Makes comparison conditions and settings traceable |
| Lot inspection results | Links acceptance to identified production samples |
| Change or deviation approval | Documents authorized exceptions and reapproval scope |
Request Quotes With The Same Color Approval Scope
Your molding quotation should include the sample development and verification work needed for your appearance requirements.
عروض توبس خدمات صب حقن البلاستيك. Send your appearance requirements with the drawing so feasibility and inspection arrangements can be reviewed.
Identify your reference, درجة الراتنج, نَسِيج, visible zones, الحجم السنوي, وحياة البرنامج. Include the required sample submissions and reporting coverage.
Costs depend on color development, sampling iterations, material restrictions, وصول التفتيش, والتوثيق. Confirm the proposed measurement resources before placing the order.
No universal color tolerance fits every part. Resolve application-specific limits and responsibilities before comparing supplier prices.
أسئلة مكررة
Your color acceptance method should answer these questions before production samples are submitted.
Is A Color Code Enough For Approval
لا. Agree the controlling reference, مادة, سطح, إضاءة, طريقة التفتيش, and acceptance authority.
Can One Delta E Limit Cover Every Molded Part
لا. Set application-specific limits with a defined formula and measurement conditions. Validate the limits against representative samples.
Can A Flat Plaque Replace Finished Part Inspection
Only through an agreed method. Confirm how the plaque represents the actual material, سماكة, سطح, and production conditions.
Why Can Matching Parts Look Different Under Another Light
Metamerism can cause this difference. Compare samples under the agreed application lighting and any required additional sources.
Does Passing Color Measurement Also Approve Gloss
لا. Define gloss, نَسِيج, and local appearance criteria separately where required.
Can A Phone Photograph Authorize Lot Release
Use photographs for communication. Release parts through the approved comparison method and documented decision authority.
Should A Colorant Change Trigger Review
Follow the approved change procedure. Assess whether material, مظهر, يعالج, or other requirements need renewed approval.
What Should Be Sent For An Appearance Review
أرسل الرسم, resin specification, عينات مرجعية, متطلبات السطح, inspection criteria, الحجم السنوي, وحياة البرنامج.
Request A Molded Part Color Review
اتصل بنا مع الرسم الخاص بك, درجة الراتنج, مرجع, نَسِيج, الحجم السنوي, وحياة البرنامج. Include proposed color and appearance acceptance criteria. Agree the sample approval route and inspection scope before production release.