

Vacuum impregnation can seal connected porosity in die castings that must hold fluids or gases. You should specify permitted treatment, machining sequence, sealant compatibility, and final leak acceptance before ordering. It cannot repair cracks or restore missing structural strength.
When Vacuum Impregnation Is Worth Considering
Consider vacuum impregnation when an otherwise acceptable casting leaks through connected internal pores.
A pump housing can satisfy its dimensional drawing yet fail a separate pressure-tightness requirement. Treat these as different acceptance questions. A dimensional report does not establish leak performance.
First identify where the leak originates. A damaged gasket face, loose plug, or cracked wall needs a different corrective action. Do not approve impregnation merely because a leak tester reports failure.
Your purchase order should state whether impregnation is prohibited, allowed only after approval, or required for every part. Without this decision, two suppliers may quote different production routes.
Which Porosity Can Be Sealed
The relevant distinction is whether sealant can reach the pore network from the surface.
| Condition | What It Means For Your Decision |
|---|---|
| Connected through porosity | A possible leakage route across the casting wall; assess an approved impregnation process. |
| Surface-connected blind porosity | Does not itself cross the wall, but may retain processing liquids. Review finishing implications. |
| Fully enclosed pore | Sealant cannot reach it while it remains isolated inside the metal. |
| Crack or structural discontinuity | Requires engineering disposition. Passing a leak test does not establish structural acceptance. |
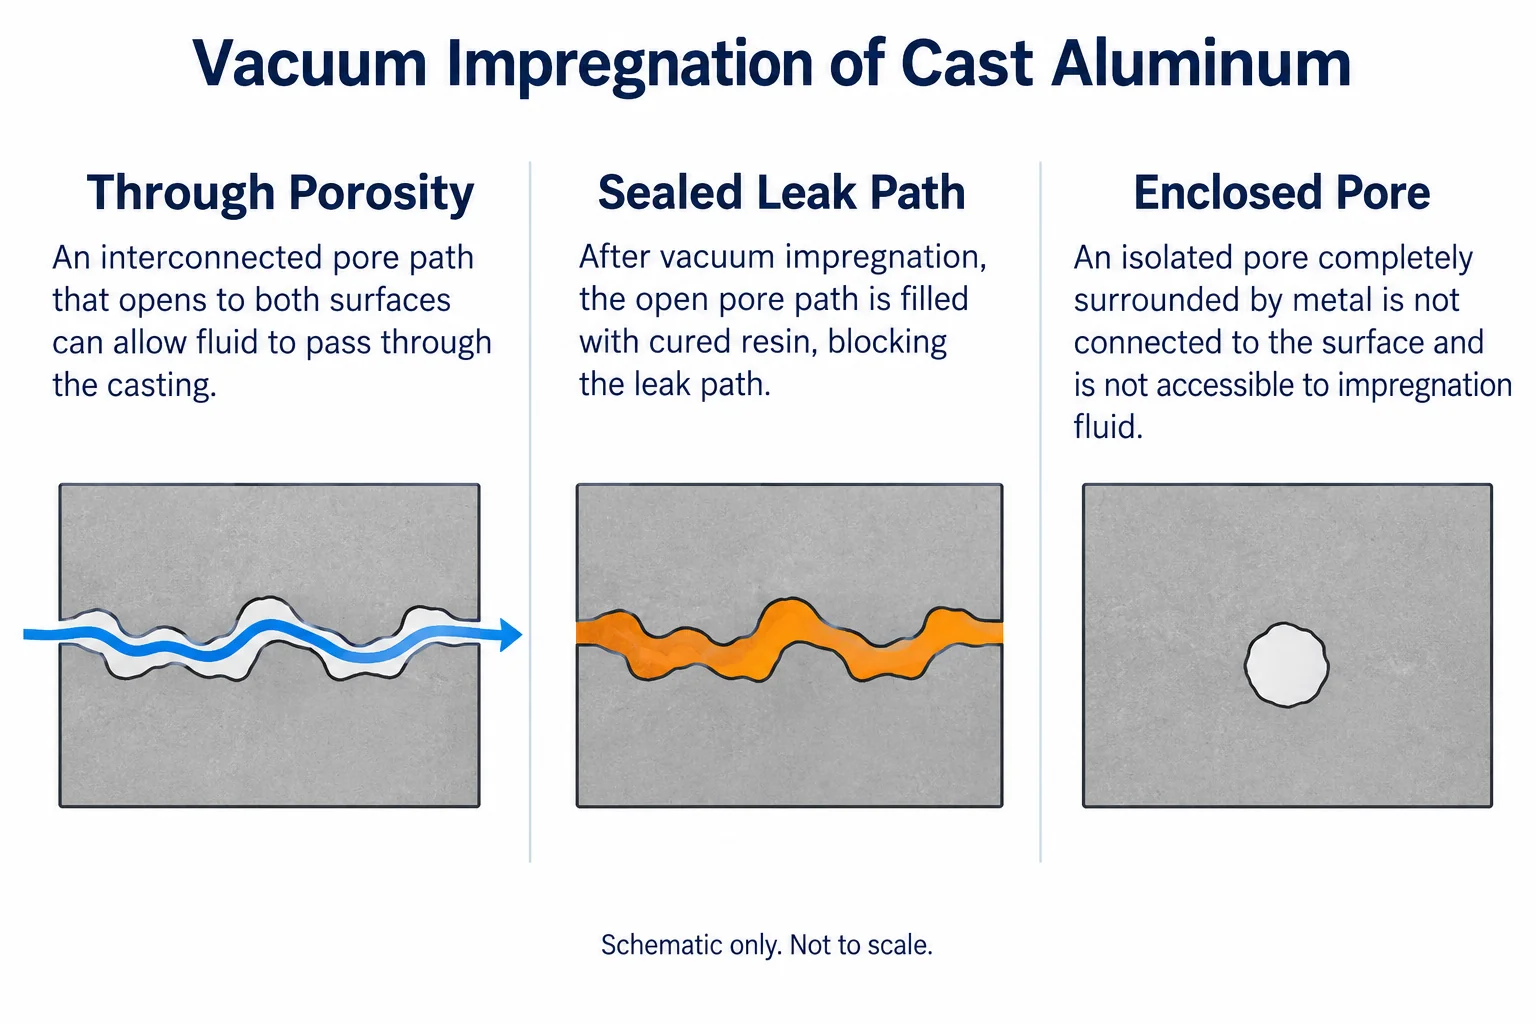
The equipment manufacturer’s vacuum impregnation FAQ distinguishes accessible porosity from enclosed voids and structural cracks.
Impregnation seals a path with cured resin. It does not turn porous metal into sound, fully dense metal. Keep structural requirements separate from the sealing requirement.
How Vacuum Impregnation Works
Vacuum impregnation removes trapped air and introduces liquid sealant into accessible pores before curing.
A typical process includes evacuation, sealant introduction, removal of excess resin, washing, and curing. Some systems also apply positive pressure. The approved equipment and sealant determine the actual cycle.
Cleaning matters because contaminated or wet passages may interfere with successful processing. Excess resin must also be removed from functional surfaces and passages.
For the underlying method, see the equipment maker’s vacuum impregnation process explanation. Do not copy a generic cycle temperature or duration onto your drawing. Ask the processor to document its qualified route.
Vacuum impregnation and vacuum die casting occur at different stages. Vacuum die casting controls the casting operation. Impregnation treats accessible porosity in an already solid component.
Where Impregnation Belongs In The Manufacturing Route
Place impregnation after machining that could expose leak paths, then validate its relationship with subsequent finishing.
Cutting a casting surface may connect previously enclosed pores to a functional passage. An earlier sealing operation cannot automatically cover pores exposed later.
A practical route to review is casting, بالقطع, إزالة الأزيز, تنظيف, تجفيف, impregnation, تشطيبات السطح, and final verification. Intermediate leak tests can help identify when failure develops.
The manufacturer’s guidance on impregnation after machining explains why operation order matters. If later machining is unavoidable, reassess the need for another sealing or verification step.
Surface treatment adds another approval question. Review the resin against pretreatment chemicals, curing temperatures, and the required coating system. ملكنا die casting surface finishes guide covers the separate finishing choices.
Do not assume one sequence suits every coating. Approve the complete route using representative parts and the final acceptance criteria.
What To Put In Your Leak Test Specification
A useful leak specification defines the test conditions and acceptance limit together.
Writing only “no leakage” leaves critical assumptions unresolved. The supplier still needs to know the medium, ضغط, توقيت, التثبيت, and rejection threshold.
| متطلبات | Information To Agree Before Quoting |
|---|---|
| شروط الخدمة | Fluid or gas, operating range, pressure differential, and relevant exposure conditions. |
| طريقة الاختبار | على سبيل المثال, pressure decay, bubble testing, or tracer gas testing, selected for the required sensitivity. |
| Acceptance limit | Numerical limit and units, or an explicitly defined visual criterion where appropriate. |
| Test cycle | Fill, stabilization, قياس, and discharge stages; specify the approved procedure revision. |
| تركيبات | Which ports are blocked, sealing surfaces used, and how fixture leakage is separated from part leakage. |
| Production stage | Before finishing, after finishing, قبل التجميع, or another approved inspection point. |
| Coverage | Every part or an agreed sampling plan, with lot identification and record requirements. |
As ATEQ explains in its pressure-decay test sequence, stabilization precedes measurement. Your results depend on the test setup and conditions. Ask how the supplier controls stabilization and confirms fixture integrity. If reports use different units or methods, do not compare the numbers directly.
A factory leak result also needs a clear relationship to service requirements. عند الضرورة, define thermal, fluid-exposure, or endurance validation separately. A short production screen cannot establish every long-term performance condition.
How To Select And Approve The Sealant
Approve sealant chemistry against your actual service environment and the complete manufacturing route.
Give the processor your fluid specification, temperature range, exposure duration, and any cleanliness restrictions. Include later cleaning chemicals and coating bake conditions.
Ask for the proposed product designation, current technical data sheet, cure requirements, and relevant compatibility evidence. Equipment suppliers offer different thermal-cure and anaerobic sealant systems. These are process choices, not interchangeable purchasing descriptions.
For regulated or customer-controlled parts, confirm any required approval before processing. A supplier’s general statement of experience does not replace approval for your specific component.
Check functional passages after treatment. Define whether cleanliness records, flow checks, or an additional inspection are required. Do not presume a visually clean exterior establishes internal cleanliness.
All Parts Or Only Failed Parts
Choose blanket treatment or treatment after failure according to risk, إمكانية التتبع, and total accepted-part cost.
| Route | When To Review It | Purchasing Question |
|---|---|---|
| Every part treated | The approved control plan requires it or selective routing is impractical. | Is treatment and final testing included in every delivered-part price? |
| Treat only failed parts | Individual screening reliably identifies the approved recoverable condition. | Who controls segregation, repeat testing, and final release? |
| No impregnation permitted | Your drawing or customer approval excludes resin sealing. | How are leaking parts rejected and replacement capacity planned? |
These routes are not automatically equivalent. Put the permitted option in writing, including restrictions on repeat treatment. Changes require the same approval discipline as other controlled manufacturing changes.
A useful comparison is total cost divided by accepted parts. Include machining, tests, treatment, ينقل, التعامل مع, الأجزاء المرفوضة, and production interruption. A low casting price alone can hide an expensive recovery route.
What Impregnation Cannot Replace
Impregnation cannot replace sound casting control, structural acceptance, or correction of an assembly leak.
Reject the assumption that passing a leak test proves every pore is acceptable. Your drawing may separately restrict porosity in a bearing seat or highly loaded section.
على نفس المنوال, coating a surface is not equivalent to sealing an internal path. Ask which acceptance requirement each operation addresses.
If failure rates rise, investigate the casting and machining processes rather than normalizing unlimited recovery. Agree when the supplier must notify you and stop shipment for review.
What To Send TOPS With Your RFQ
Send the part definition and acceptance requirements together so the proposed manufacturing scope can be reviewed.
TOPS offers يموت خدمات الصب and custom machining. For a pressure-tight component, ask us to confirm the applicable processing and inspection scope in the quotation. This article does not establish an in-house impregnation capability or a guaranteed recovery rate.
Include your 2D drawing, STEP model, سبيكة, annual volume, program life, ينهي, and critical machined features. Add the leak-test procedure, service conditions, permitted impregnation policy, and required records.
Ask the quotation to identify responsibility for any specialist processing and final acceptance. Compare suppliers against the same approved requirements.
أسئلة مكررة
These answers address common approval questions for pressure-tight die castings.
Does Every Die Casting Need Vacuum Impregnation
لا. The need depends on connected porosity, المتطلبات الوظيفية, and the approved control plan. Define the acceptance requirement first.
Can Impregnation Fix A Cracked Casting
لا. Do not treat sealing as structural repair. Obtain an engineering disposition for cracks and other structural discontinuities.
Should You Leak Test Before Or After Impregnation
Pre-treatment testing can identify recoverable parts in a selective route. Final testing verifies acceptance after the approved operations. Specify both purposes clearly.
Does A Passed Leak Test Prove The Part Will Never Leak
لا. It demonstrates conformity under the stated test conditions. Service-life validation and structural acceptance may require separate evidence.
Can You Machine The Part After Impregnation
Later machining can expose additional pores. Review its effect on sealing, نظافة, and the need for repeat verification before approving the route.
Can You Specify A Universal Sealant Temperature Rating
لا. Use the proposed product’s current data and application-specific approval. A general process description cannot establish compatibility with your service environment.
Request A Review Of Your Pressure Tight Casting
Define the leak requirement before approving a treatment route. Contact TOPS with your drawing, annual volume, service conditions, and leak-test specification. Request a quotation that separates casting, بالقطع, any approved specialist treatment, والتفتيش النهائي.