

Your nitriding specification for steel parts should define material condition, treated surfaces, hardness measurement, 深さ, および受理証拠. A process name or surface hardness number alone leaves important requirements unresolved. Agree the verification plan before machining and treatment, especially when inspection requires sectioning a part.
Identify The Steel And Its Starting Condition
Your nitriding order should identify the exact steel grade and condition entering treatment.
Include the material standard, 学年, prior heat treatment, and required core properties. The treatment response depends on the substrate. A supplier cannot establish equivalent results from an unspecified “steel” description.
Define the surfaces requiring treatment and any areas requiring protection. Mark critical wear faces, スレッド, bearing locations, and inspection positions. Include restrictions on subsequent polishing, 研削, or material removal.
Nitriding enriches the surface with nitrogen. It changes the near-surface material rather than adding a conventional paint film. Confirm the selected process route and its suitability for your steel and functional requirements.
Specify The Layer Characteristics Separately
Your drawing should distinguish surface hardness, nitriding hardness depth, and any compound layer requirements.
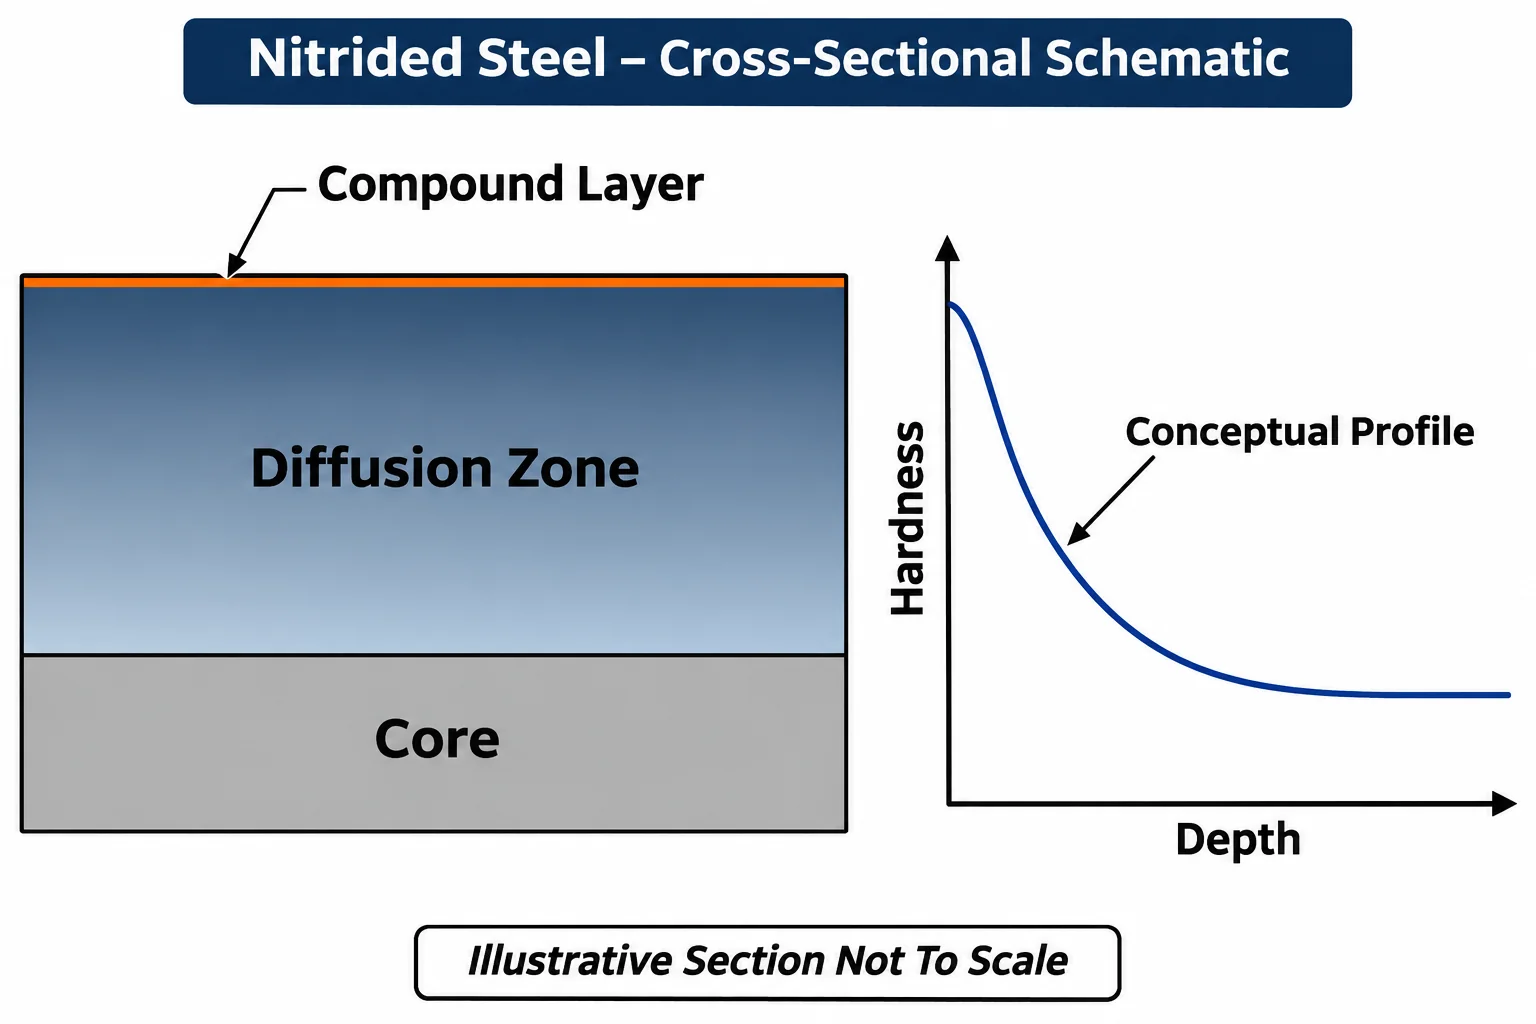
The compound layer and the underlying diffusion zone describe different regions. Their presence and characteristics depend on material and process conditions. ASM International explains the nitriding zones.
A high surface hardness result does not establish the required depth. 同じく, a depth result alone does not establish acceptable surface structure. Define each characteristic your application needs instead of treating them as interchangeable.
Use precise terminology for the depth measurement. ISO 18203 2026 covers determining several surface-hardened layer depths, including nitriding hardness depth. Identify the agreed standard edition and applicable definition. Avoid an unexplained “case depth” note that buyer and supplier interpret differently.
Do not adopt a universal layer thickness or hardness target from another part. Your design authority should establish limits for the actual material and service conditions.
Match The Hardness Method To The Treated Layer
Your acceptance requirement should state the hardness method, 規模, test force, and measurement location.
A reading without its method and load cannot be interpreted reliably. A bulk indentation method may sample material beneath a thin treated region. Confirm that the selected procedure can assess the characteristic you intend to control.
Do not convert an unexplained Rockwell result into a claimed microhardness profile. Different methods and sampling volumes can answer different questions. Ask the laboratory to justify the method for the layer and specimen geometry.
A file check or visible surface finish cannot replace the agreed hardness test. Use the specified measurement procedure and retain the actual results.
Agree Destructive Sampling Before Production
Your inspection plan should define whether verification uses finished parts, representative coupons, または両方.
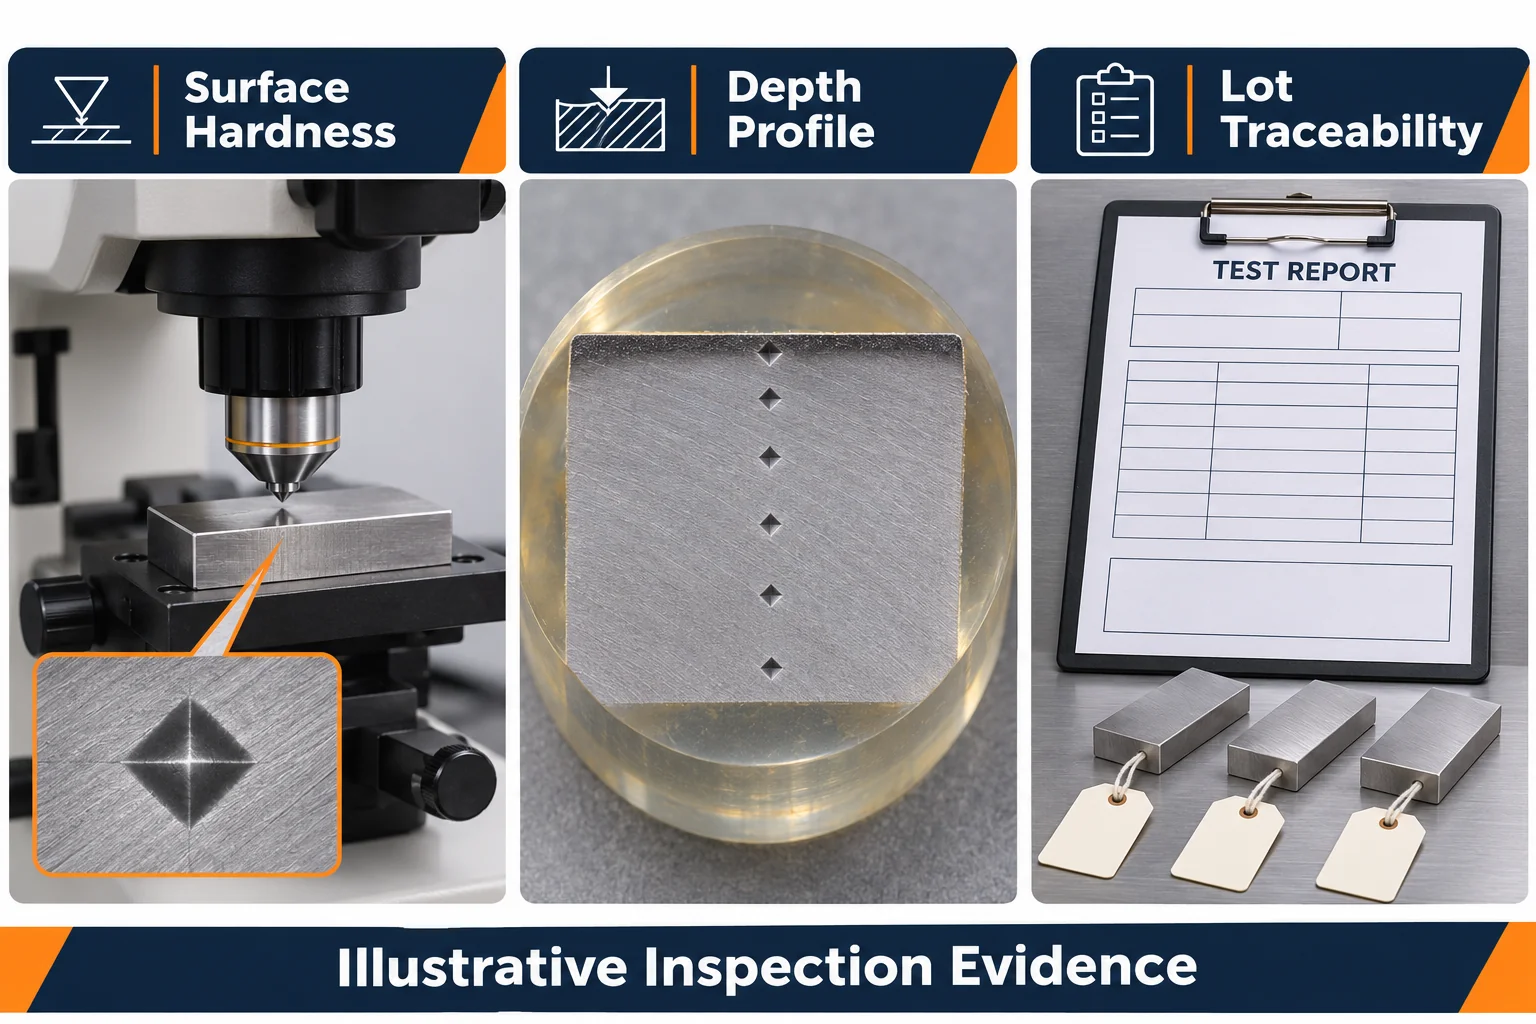
A hardness depth evaluation commonly uses a prepared cross-section and measurements into the material. Define where the section is taken and how the relevant surface is preserved. Identify the measurement path and required reporting detail.
Struers discusses preparing nitrided components, including edge retention and preparation damage. A rounded or damaged specimen edge can undermine assessment of a shallow layer.
If you approve witness coupons, document their representativeness. Match the material condition and relevant treatment exposure. Agree how coupon identity connects to the production load. A convenient sample does not automatically qualify every surface on every part.
Set sampling frequency and lot definition before quoting. Include replacement parts or sample allowances when testing consumes product. Clarify who approves deviations and whether shipment must wait for test results.
Control Final Dimensions And Subsequent Operations
Your acceptance plan should verify critical geometry in the final delivered condition.
Do not assume treatment leaves every dimension unchanged. Review critical fits, 平坦さ, 表面仕上げ, and distortion allowances with the proposed supplier. Inspect the features required by your drawing after the agreed final operation.
If grinding or polishing follows nitriding, define the permitted removal and remaining layer requirements. A test performed before material removal may not describe the delivered wear surface.
Keep process corrections subject to engineering review. Additional treatment time is not automatically an acceptable repair. Review the layer, core condition, 寸法, and application requirements before approving reprocessing.
Require A Traceable Acceptance Report
Your report should link the measured results and inspection locations to the treated production lot.
| 要件 | Define Before Treatment | Evidence To Receive |
|---|---|---|
| 材料 | Grade and starting heat treatment | Material and lot identity |
| Coverage | Treated and protected surfaces | Approved drawing revision |
| 硬度 | 方法, 規模, force, locations, 限界 | Actual readings and test details |
| 深さ | 意味, procedure, section location | Depth result and supporting profile |
| 構造 | Compound layer requirements where needed | Prepared section observations |
| Final Condition | Geometry and permitted post-processing | Final inspection and disposition |
Request actual values rather than a certificate stating only “nitrided.” Include sample identifiers, inspection dates, applicable procedures, と偏差. Agree whether profile readings and section images accompany the report.
When results disagree, first compare locations, メソッド, 標本の準備, and depth definitions. Preserve the evidence before deciding on rework or rejection.
Compare Supplier Quotes With The Same Verification Scope
Your quotation comparison should include treatment, masking, サンプル, laboratory work, そして最終検査.
TOPSプレシジョンが提供する CNC加工サービス. Submit your nitriding and verification requirements during manufacturing review. Confirm the proposed treatment arrangements and reporting scope for your particular steel component.
Testing effort and destructive samples can affect cost and delivery. Separate initial qualification from recurring lot acceptance. Do not assume a low treatment price includes your required evidence.
よくある質問
Your decision should address the complete treated condition rather than one surface reading.
Does Surface Hardness Prove Nitriding Depth
いいえ. Define and verify the depth separately using the agreed measurement procedure.
Can You Accept A Coupon Instead Of A Finished Part
Only when your approved plan establishes its representativeness. Record its material, 状態, treatment connection, and permitted scope.
Can You Grind A Nitrided Wear Face Without Review
Material removal can change the delivered layer. Agree the remaining requirements and verification before approving the operation.
Request A Nitrided Part Review
お問い合わせ with your steel grade, 描画, treatment requirements, 量, and inspection criteria. Identify critical wear surfaces and permitted sampling. Agree the acceptance plan before releasing production.