



Thread plating allowance is the dimensional space you reserve before depositing a coating on a machined thread. Define the coating and finished fit together. Then agree machining limits and final inspection. さもないと, a thread that passes before plating may become too tight during assembly.
Conceptual threaded parts and gauges. Color does not identify a coating; not actual TOPS production.
Why Plating Changes Thread Fit
蒸着されたコーティングがねじ山側面のスペースを占有し、嵌合コンポーネント間の隙間を減少させます。.
外部スレッド上, 材料を追加すると有効ねじサイズが増加します. ネジ穴の内側, 堆積した材料により利用可能なスペースが減少する. 両方のコンポーネントをメッキすると、アセンブリの両側のクリアランスが消費される可能性があります.
ねじ山の側面がかみ合いを確立するため、ピッチ直径が重要です. Measuring only an external major diameter cannot establish final functional fit. Your inspection plan needs to address the specified thread geometry.
弊社の machine screw thread design guide for basic terminology. This article focuses on deposited coating and acceptance after finishing, rather than general thread design.
Estimate Thread Build Up Without Treating It As A Guarantee
For an ideal 60-degree thread, uniform deposited flank thickness changes pitch diameter by approximately four times that thickness.
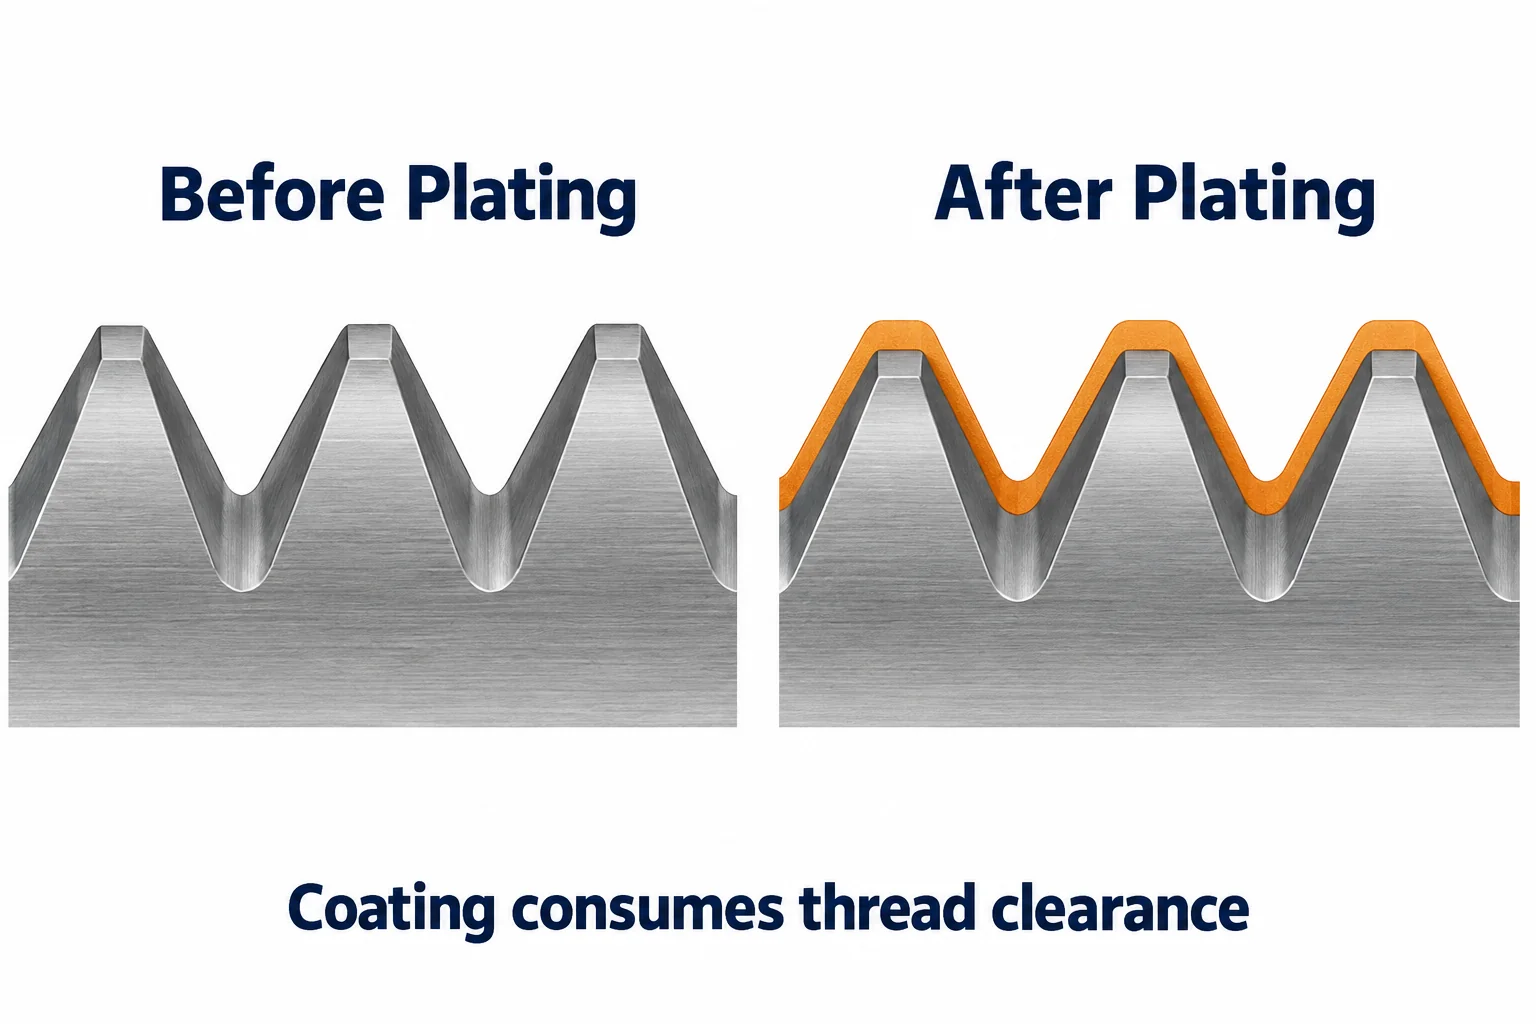
Thread Check’s technical catalog explains this 4:1 relationship for common 60-degree threads. It is a geometric planning relationship, not a complete machining or gauge specification.
例えば, 均一に堆積された厚さを仮定すると、 5 おねじの側面でマイクロメートル. ピッチ直径の推定増加量は次のとおりです。 20 マイクロメートル, または 0.020 んん.
例示的なプロセスでは、代わりに局所的に 5 ~ 8 マイクロメートルが堆積する場合, 対応する推定増加幅は 20 ~ 32 マイクロメートル. これらの発明された厚さの例は計算を説明しています; 推奨されるコーティング仕様ではありません.
許容される開始寸法は、実際のねじの制限とコーティングの分布を考慮する必要があります。. すべてのねじ寸法から 1 つの公称値を単純に減算しないでください。.
めねじ用, 材料の堆積により、利用可能なピッチ直径が減少します. 各成分を個別に計算するのではなく、嵌合ペアを確認する.
Keep The Formula Within Its Scope
この関係は、指定されたプロファイルと関連する側面への均一な堆積を前提としています。. 実際のコーティングの厚さは位置や形状によって変化する可能性があります.
同じ推定値を管用テーパーねじに自動的に適用しないでください。, 他の側面角度, または変換治療. 陽極酸化には、蒸着金属メッキとは異なる成長挙動が含まれます。. 寸法を個別に確認してください.
Define The Finished Thread Before Choosing Machining Limits
図面では、最終的な合格要件と、コーティング前の機械加工を制御するために使用される寸法を区別する必要があります。.
| 要件 | 指定する内容 | なぜそれが重要なのか |
|---|---|---|
| スレッド ID | 標準, 呼び径, ピッチ, 利き手, とスレッドクラス | 必要な形状とフィット感を確立します |
| 受入条件 | 完全なフィニッシュシステム後に制限が適用されるかどうか | 検査時期に関する意見の相違を防ぐ |
| コーティングシステム | 蒸着金属, 厚さの範囲, 後処理, および関連する表面 | 評価する寸法変化を定義します |
| 相手部品 | そのスレッドクラス, 仕上げる, と噛み合いの長さ | クリアランスは組み立てられたペアに属します |
| 検査 | 必要なゲージ, メソッド, カバレッジ, and reporting | Makes acceptance measurable |
For ISO metric fasteners, review the applicable requirements in ISO 4042. Its scope concerns electroplated coating systems for fasteners; it does not automatically govern every custom threaded component.
State the contractually required edition and amendments. Avoid substituting a catalog summary for the applicable specification.
Do Not Assume A Thread Class Covers Any Coating
A tolerance designation may provide allowance, but its suitability depends on size, ピッチ, コーティング, and final requirements. Small or fine threads can have limited dimensional space.
Bossard’s corrosion-protection resources include coating-thickness guidance for ISO metric threads. Use the relevant technical data with your drawing and process review.
Choose Between Compensation Masking And Later Machining
Choose the production route according to where coating is required and how the finished assembly must function.
| Route | When To Evaluate It | Limitation To Resolve |
|---|---|---|
| Machine with approved coating allowance | Threads must retain the specified deposited coating | Local thickness and starting limits need control |
| Mask the thread during coating | An uncoated thread is permitted | Coverage boundaries and corrosion protection need approval |
| Machine the thread after coating | Final machining is permitted by the design | Cutting removes coating from affected surfaces |
| Revise the finish or fit | The original coating and thread limits are incompatible | Engineering approval and assembly validation are needed |
Masking should be a drawing decision, not an undocumented shop-floor workaround. Identify the masked surfaces and acceptable boundary condition.
Cutting or chasing a plated thread can expose base metal and create debris. It may change corrosion performance or violate the coating requirement. Require approval before treating it as a repair.
For general finish background, 私たちのを参照してください zinc plating guide. The required corrosion protection and thread fit must remain compatible.
Coordinate The Machine Shop And Plating Supplier
Both suppliers need the same finished-thread requirements and an agreed method for controlling coating variation.
Send the coating specification during quotation rather than adding it after machining. Identify blind threaded holes, deep engagement, small diameters, and surfaces needing special attention.
Ask where thickness will be measured and how that location represents the functional thread. A measurement on an accessible flat surface may not describe deposition deep inside a hole.
Agree how parts will be handled, 掃除, 保護された, and identified across outside processing. Link coating records and inspection reports to the actual batch.
For high-strength steel, also review applicable hydrogen-embrittlement controls with the finishing specialist. A satisfactory thread-fit result does not establish compliance with every material or coating requirement.
Inspect The Thread After The Complete Finish
Final inspection should verify the specified thread condition after all finish steps that affect the delivered component.
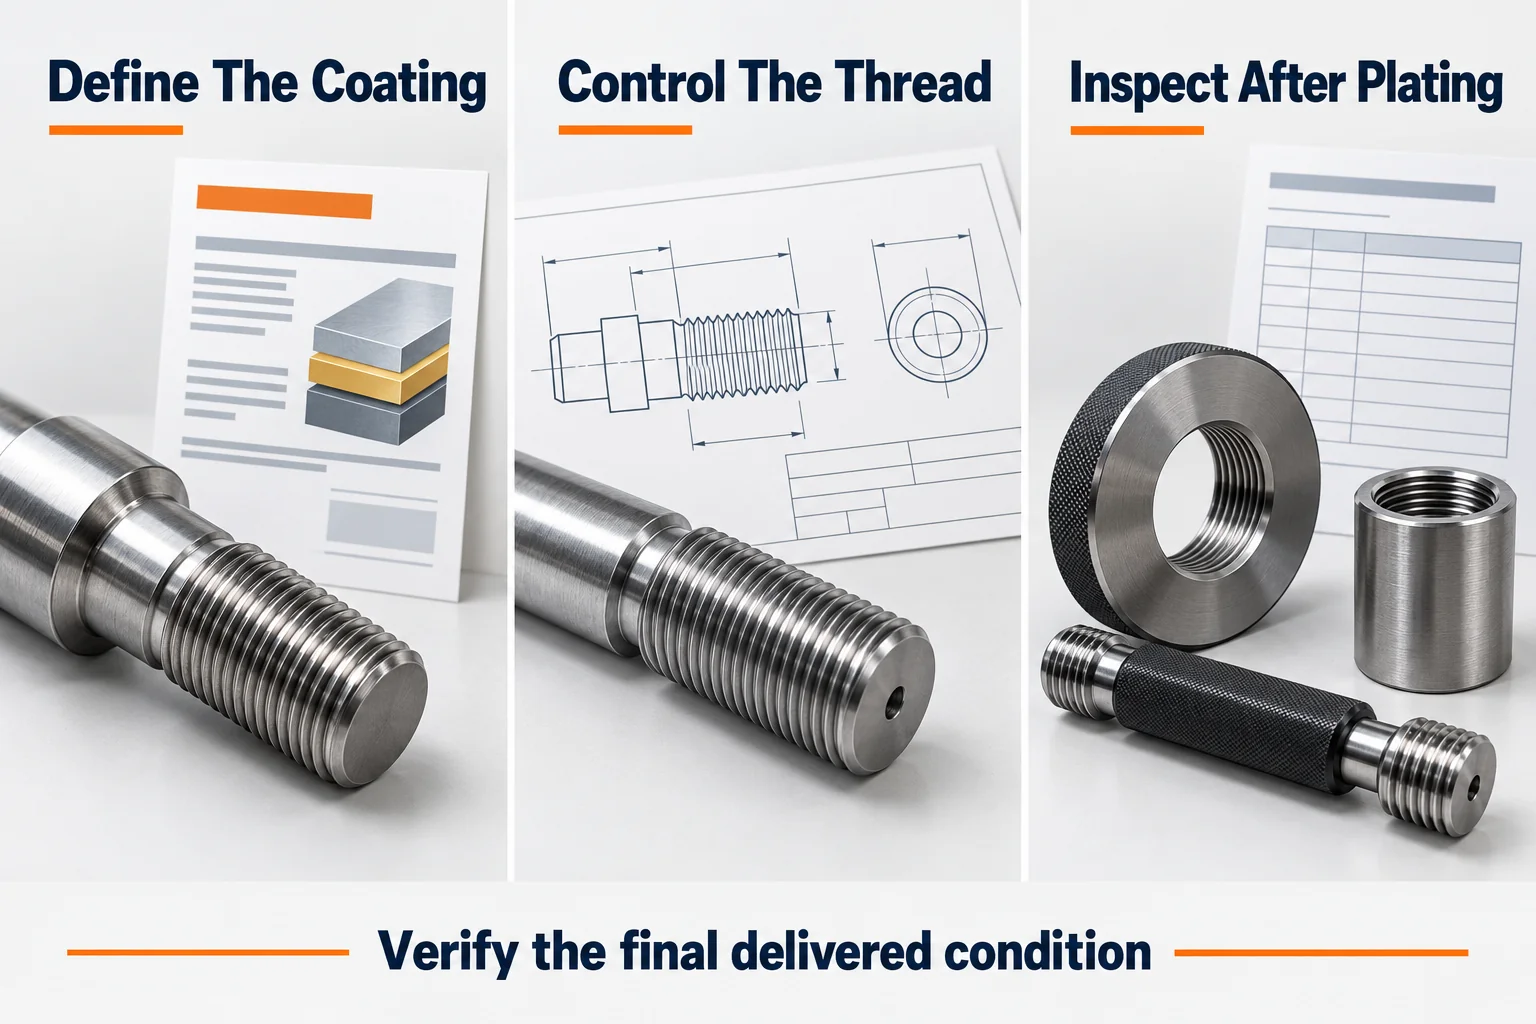
Use the appropriate calibrated thread gauges and acceptance procedure for the drawing. Distinguish pre-plating process gauges from final acceptance gauges. Their purposes and limits may differ.
Do not force a gauge into a tight thread. Investigate coating buildup, バリ, 汚染, profile errors, or damage before changing the process.
| チェック | Evidence It Provides | 重要な制限 |
|---|---|---|
| Pre-plating thread measurement | Control of the machined starting condition | Does not establish final fit |
| Coating-thickness measurement | Deposit thickness at measured locations | May not represent every thread flank |
| Final thread gauging | Conformance within the selected gauge procedure | Does not establish coating adhesion or corrosion life |
| Representative assembly test | Fit with the specified mating component | Does not replace dimensional acceptance |
Define sampling or complete inspection according to risk and the agreed quality plan. Retain identified samples when they support process approval. Revalidate relevant changes to material, coating supplier, or machining limits.
メッキねじがきつくなった場合の対処方法
Investigate the starting dimensions, coating condition, and acceptance method before selecting a corrective action.
初め, confirm the drawing revision, thread identity, and gauge condition. Then compare pre-plating records with final measurements and the coating report.
Inspect the entrance, thread flanks, and engagement length for roughness, nodules, チップ, または損傷. Check whether both mating parts received an unaccounted coating.
Contain affected parts while the cause is reviewed. Any stripping, replating, or thread rework needs approval against dimensional and material requirements. Do not assume a nut running onto one sample establishes batch acceptance.
ねじのめっき代に関するよくある質問
Thread allowance must follow the specified profile, コーティングシステム, and finished acceptance condition.
めっきの厚さはピッチ直径の成長と同じですか
いいえ. For ideal uniform deposition on common 60-degree threads, estimated pitch-diameter change is approximately four times flank thickness. Confirm applicability before setting machining limits.
雌ねじにメッキを施すことはできますか
It may be feasible, but coverage and dimensional control depend on geometry and process. Ask the finishing supplier to review depth, アクセス, 厚さの要件, and inspection locations.
メッキ前にゲージに合格すると最終的なフィット感が保証されますか
いいえ. Coating changes the finished geometry. Inspect again after the required finishing sequence using the agreed final acceptance method.
ネジ穴を常にマスクする必要があるか
いいえ. Mask only when the design permits an uncoated thread and defines acceptable boundaries. Some applications require protective coating on those surfaces.
メッキ後にネジ山を追うことはできますか
Only with an approved process that preserves the required final condition. Chasing can remove coating and create contamination. Review corrosion and dimensional consequences first.
TOPS にメッキ CNC スレッドのレビューをリクエストする
You can ask TOPS to review machining and finishing requirements together for your custom threaded component.
私たちの CNC加工サービス cover custom milled and turned parts. Confirm the coating route, supplier responsibilities, and final inspection scope for your project.
Send the drawing, 材料, thread specification, コーティングシステム, mating-part information, and order quantity. Identify final acceptance requirements and any masking restrictions.
Request A Threaded Part Review to discuss the machining allowance, 仕上げシーケンス, inspection plan, and quotation together.

