Die casting flash acceptance needs defined locations, measurable residue limits, and an agreed inspection method. “Remove flash” alone leaves too much interpretation. You should distinguish functional surfaces, handling edges, and appearance areas before approving tooling or comparing production quotes.
Identify What The Inspector Is Evaluating
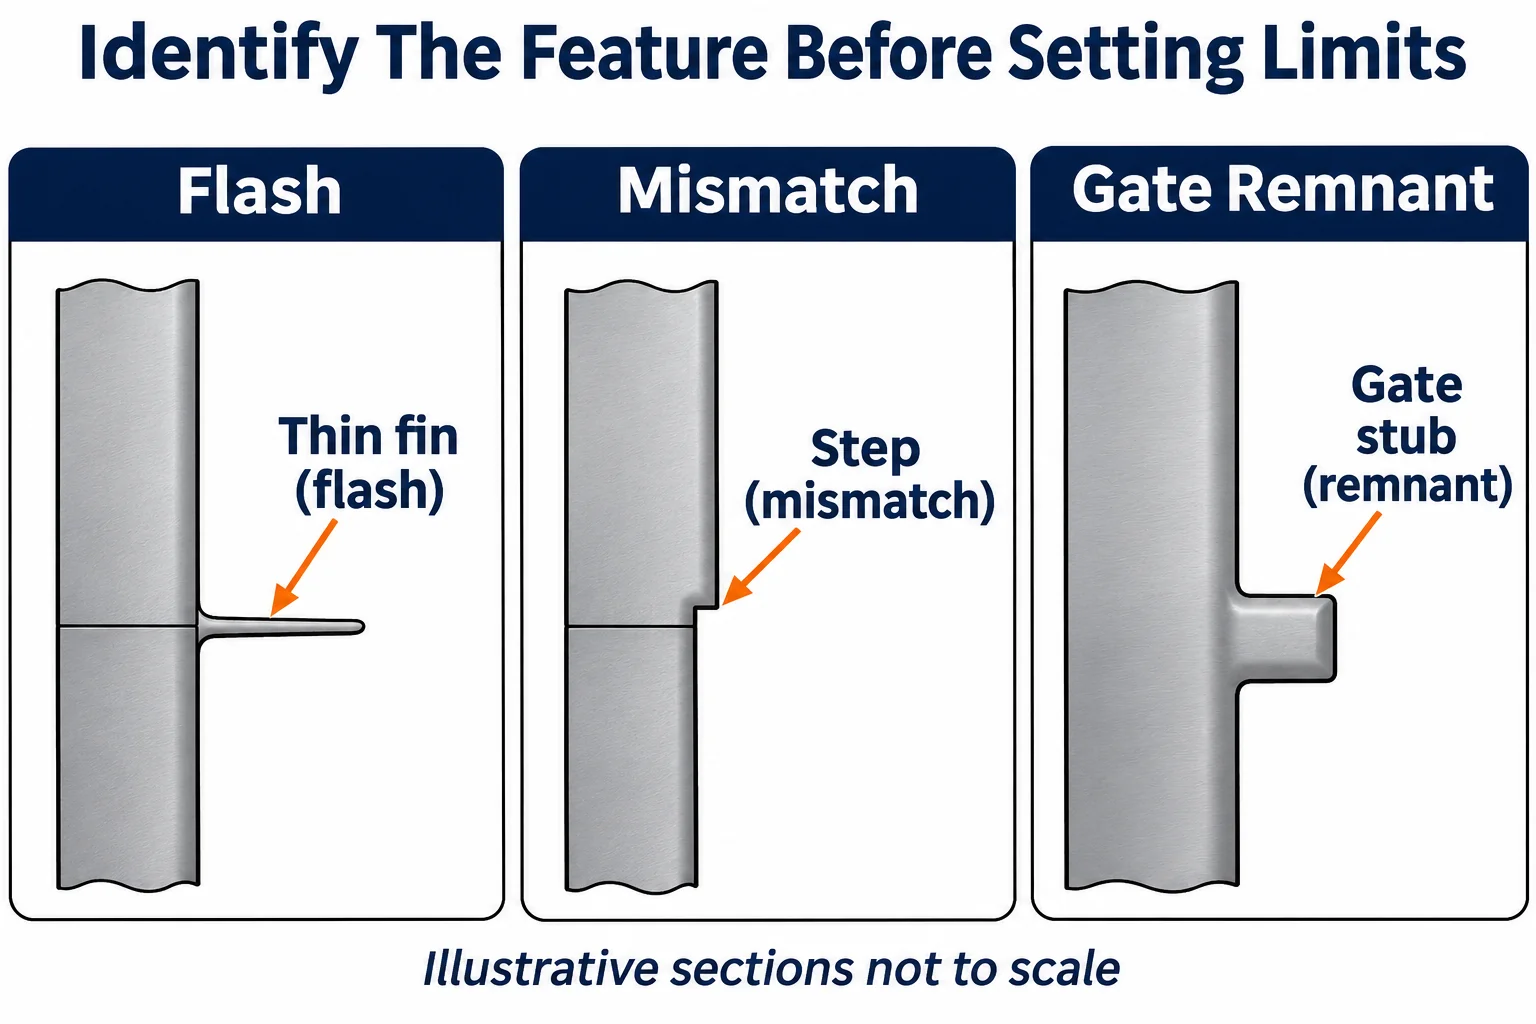
Flash is excess metal at a die interface, while mismatch and gate remnants describe different features.
A thin fin can remain near a parting seam. Mismatch creates a step between adjoining contours. A gate remnant comes from the metal feed connection.
Removing a fin does not necessarily correct a contour step. Agree separate limits where these features affect assembly or appearance.
NADCA’s parting line guidance connects die layout with flash formation and trimming access. Review the proposed parting line before freezing the casting drawing.
Set Flash Limits By Functional Zone
Your acceptance limits should follow the consequences of remaining metal at each location.
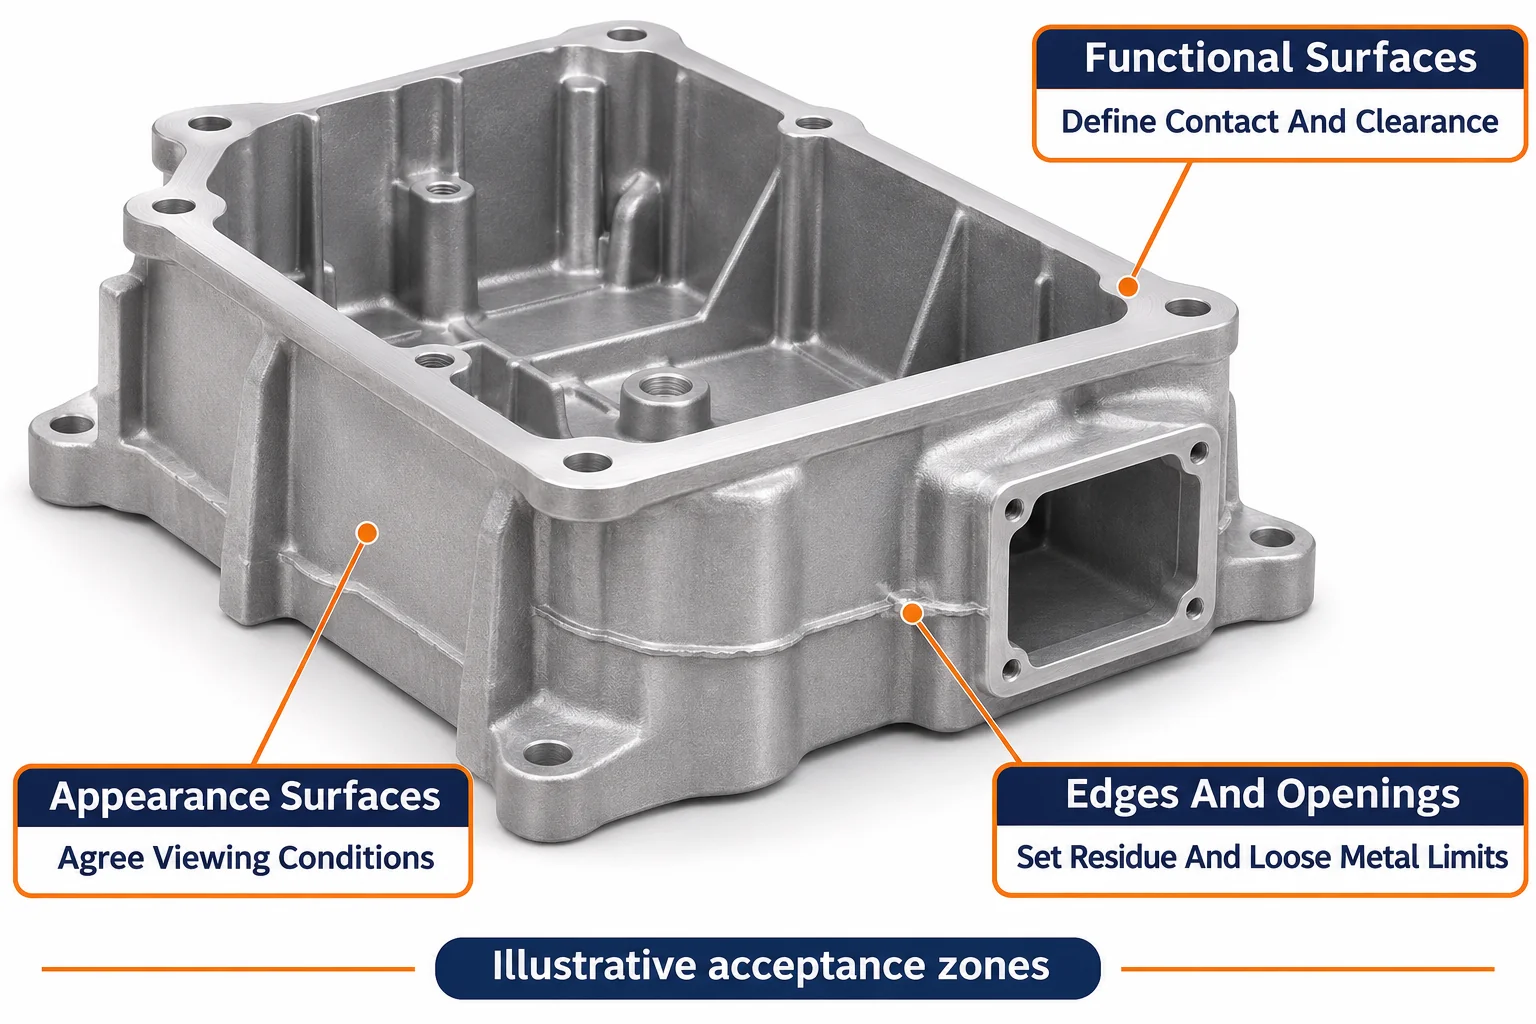
A noncontact exterior seam can have different requirements from a gasket seat or sliding interface. Mark the actual zones on the drawing.
| Zona | Risk To Review | Acceptance Information |
|---|---|---|
| Sealing or mounting face | Interrupted contact or assembly interference | Permitted residue and required surface condition |
| Hole or opening | Reduced clearance or obstructed passage | Inspection location and usable opening requirement |
| Handling edge | Sharp projection or loose fragment | Edge condition and loose material criterion |
| Appearance surface | Visible seam or trimming mark | Viewing conditions and approved boundary sample |
| Nonfunctional seam | Unnecessary finishing expense | Agreed remaining extension and inspection method |
Specify the geometry being measured. Flash projection, grossura, and mismatch are different quantities.
Define the reference surface, measurement direction, and maximum permitted extent where relevant. Avoid a single limit that cannot be measured consistently.
Define The Required Removal Operation
Your purchase order should distinguish gate removal, flash trimming, and any additional finishing needed for acceptance.
The International Zinc Association’s trimming guidance explains how trim dies remove gates, transborda, and flash. It also warns that barrelling can bend some flash instead of removing it.
Ask which features the proposed operation reaches. Internal openings and complex parting lines can require different access or secondary work.
Do not assume that a trimmed casting has a polished seam. Specify any required blending, usinagem, edge treatment, or loose material removal separately.
Agree allowable parent-metal removal. Overprocessing can change a critical edge, contact surface, or remaining wall.
Agree Inspection Conditions Before Sampling
A repeatable inspection plan defines where, como, and at what production stage flash acceptance is checked.
Use direct measurement where practical. For subjective appearance decisions, agree lighting, viewing distance, orientação, and approved samples.
The International Zinc Association’s quality specification guidance recommends measurable critical requirements and agreement on subjective assessments.
| Verificar | Informações para concordar |
|---|---|
| Localização | Drawing zone, seam segment, opening, or contact surface |
| Método | Suitable measurement tool, acessório, or visual comparison |
| Condition | After trimming, Após a usinagem, or after final coating |
| Amostragem | Production lots, cavidades, frequency, and escalation rules |
| Decision | Critérios de aceitação, records, and approval responsibility |
Check representative cavities and difficult trimming locations during qualification. A convenient exterior edge cannot represent every internal seam.
Keep external flash acceptance separate from internal casting inspection. Surface cleanup does not establish internal soundness.
Use Standards And Samples Precisely
A standard or sample becomes useful when your agreement identifies its scope, revisão, and applicable features.
NADCA’s product specification standards overview covers design, tolerâncias, e garantia de qualidade. Identify the relevant document edition and requirement instead of writing only “to NADCA.”
A photographed sample can clarify appearance. Include scale, orientação, zone identification, and the decision it illustrates.
Retain approved boundary samples with revision control. An unusually clean prototype should not silently become an unsupported production requirement.
Compare Quotes On The Same Acceptance Basis
Your quote comparison should include the trimming route, operações secundárias, Inspeção, and permitted rework.
Costs depend on parting-line access, ferramentas, manuseio, parent-metal protection, and inspection effort. Tighter requirements need justification at the affected locations.
Ofertas TOPS Serviços de fundição de matriz. Share the marked drawing and finish requirements so the proposed casting and removal route can be reviewed together.
Ask which operations and verification records are included. Confirm approval requirements for changes to trimming, acabamento, or rework.
For recurring loose metal or increasing residue, investigate the source before adding repeated manual cleanup. Keep accepted dimensions and functional requirements unchanged.
perguntas frequentes
Your specification should resolve common interpretation gaps before production approval.
Is Every Visible Parting Line A Reject
Não. A witness line can remain after trimming. Acceptance depends on the drawing, função, and agreed appearance criteria.
Are Flash And Die Mismatch The Same
Não. Flash is excess metal. Mismatch is a contour offset, which needs its own evaluation and limits.
Does Gate Removal Include Complete Deflashing
Not automatically. Specify the required operations and the permitted condition at each relevant feature.
Can Tumbling Remove All Flash
Não. Results depend on the feature and process. Some thin extensions can bend over, so verify the actual part.
Should I Specify Zero Flash Everywhere
Only where justified and agreed with a defined inspection method. Specify functional requirements rather than an unmeasurable blanket statement.
Can Coating Hide An Unacceptable Seam
Do not rely on coating to correct nonconforming geometry. Agree both prefinish and final appearance requirements where needed.
Does An Approved Sample Replace Dimensions
Não. Use samples for the agreed attributes while retaining measurable drawing requirements and revision control.
What Should A Trimming RFQ Include
Send CAD, a marked drawing, liga, quantidades, volume anual, vida do programa, terminar, limites de aceitação, e requisitos de inspeção.
Request A Flash Acceptance Review
Contate-nos com seu desenho, liga, volume anual, e programar a vida. Mark critical seams, openings, and appearance zones so removal and inspection requirements can be agreed before tooling approval.