



Инжекционното формоване с тънки стени произвежда леки пластмасови части чрез запълване на тесни секции, преди стопилката да загуби способността си да тече. Success depends on flow distance, resin grade, инструментална екипировка, and machine response. This guide explains how you can assess feasibility, control defects, and compare costs before committing to a mold.
What Is Thin Wall Injection Molding?
Thin wall injection molding addresses parts whose narrow sections create demanding filling and process-control requirements.
There is no single wall thickness that defines every application. A short flow path in one resin can be manageable. A longer path at the same thickness can be difficult.
You therefore need more than a minimum-wall number. Evaluate the complete geometry, selected grade, gate arrangement, and production system.
Thin-wall packaging and technical housings also have different priorities. A container may prioritize weight and stacking. A housing may prioritize flatness, Устойчивост на въздействие, and assembly fits.
Neither category justifies a universal cycle time, толерантност, or machine-speed specification.
Why Does The Flow Length-To-Thickness Ratio Matter?
The flow length-to-thickness ratio helps describe how far the melt must travel relative to the available wall section.
For a simplified uniform wall, calculate L/t using the same units. L is the flow path from the gate toward the last-filled region. It is not necessarily the part’s overall length.
For illustration, а 100 mm path through a 1 mm wall gives L/t = 100. При 0.5 мм, the same path gives L/t = 200. These are arithmetic examples, not recommended design limits.
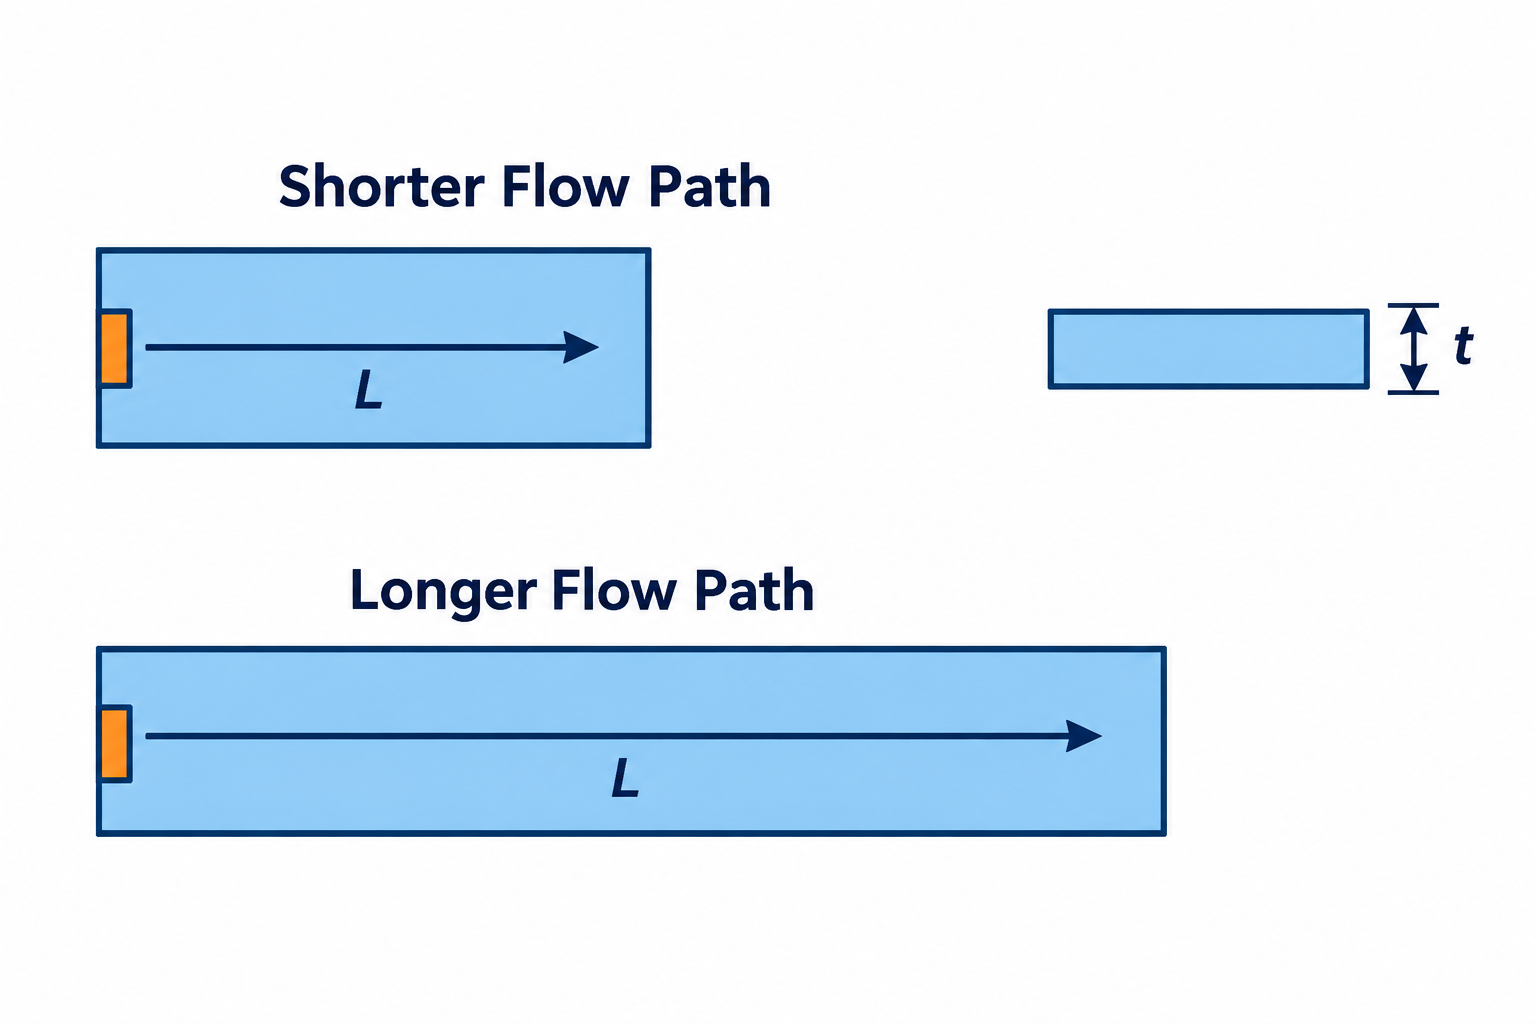
Figure 2. Flow length L and wall thickness t must be considered together. Simplified schematic, not to scale.
Reducing thickness can increase filling difficulty even when the part’s external dimensions stay unchanged. Local restrictions, corners, and changes in thickness complicate the comparison further.
Use L/t as a screening measure, not a pass/fail standard. BASF’s molding-analysis example evaluates flow length, дебелина на стената, материал, and injection location together.
Ask your supplier how the proposed gate and grade affect the actual filling path. A high-flow resin does not automatically overcome every restriction.
How Does Thin Wall Molding Differ From Conventional Molding?
Thin wall molding usually places greater emphasis on filling dynamics and maintaining a repeatable operating window.
The comparison below describes tendencies. It does not define fixed boundaries between two entirely separate processes.
| Design Or Process Issue | Thin-Wall Emphasis | What You Should Confirm |
| Пълнеж | Limited time before thin sections restrict flow | Available pressure and flow rate throughout filling |
| Инструментална екипировка | Control of deflection, обезвъздушаване, and cavity consistency | Local wall variation and tool support |
| Материал | Flow behavior must balance end-use properties | Точна оценка, not only polymer family |
| Охлаждане | Thin walls may cool quickly; local thick features can dominate | Actual ejection readiness and temperature balance |
| Боравене | Lightweight walls may deform during release or transport | Ejection support, автоматизация, и опаковка |
| Economics | Material savings may offset higher equipment or tool demands | Cost per accepted part at realistic volume |
Do not infer production capability from machine tonnage alone. The injection unit and mold must also match the application.
Which Materials Are Suitable For Thin-Wall Parts?
Choose a grade that can fill the geometry while meeting the finished part’s mechanical and environmental requirements.
A resin that flows easily may not provide the required impact resistance or long-term stiffness. Evaluate both processing and service performance.
| Материално семейство | Candidate Applications | Main Selection Checks |
| ПП | Контейнери, lids, and lightweight functional parts | Flow, въздействие, скованост, температура, and shrinkage |
| PS | Selected rigid packaging and presentation parts | Бритълност, impact requirements, and grade-dependent clarity |
| ABS or PC/ABS | Slim housings and covers | Flow, външен вид, въздействие, and applicable flame requirements |
| настолен компютър | Tough housings or transparent components | Сушене, поток, остатъчно напрежение, химикали, and optical requirements |
| PA or PBT | Thin engineering features and electrical components | Влага, reinforcement, dimensional change, and service conditions |
| LCP or other specialty grades | Selected small, demanding technical components | Directional properties, weld strength, геометрия, и цена |
These are starting candidates rather than interchangeable materials. A supplier must confirm the exact grade and application requirements.
Melt flow rate can help compare grades tested under equivalent conditions. It does not fully represent viscosity during rapid cavity filling.
Use rheological data, supplier processing guidance, and trials where necessary. Avoid selecting from a single flow-index number across unrelated polymers.
For moisture-sensitive grades, define drying and material-transfer controls. Incorrect preparation can compromise quality even when the cavity fills completely.
What Design Rules Make Thin Walls More Practical?
Design the flow path, structural support, and release method together instead of simply reducing every wall.
Keep Transitions Manageable
Aim for consistent walls where function permits. Use gradual transitions and review local restrictions along the filling path.
Thick ribs, шефове, or corners can still create sink or extend cooling. Thin nominal walls do not remove these local problems.
Avoid copying one rib-to-wall ratio into every design. Материал, завършек, скованост, and molding conditions influence the acceptable geometry.
Add Stiffness Through Shape
Ребра, edge returns, and curvature can improve rigidity without uniformly increasing thickness. They must still allow filling, охлаждане, и изтласкване.
Review how the part behaves in use. A lightweight tray that fills well can still buckle during stacking or distort during sealing.
Place Gates Around Function And Flow
Compare locations that shorten difficult flow paths while protecting visible and functional surfaces. Assess meeting fronts around holes and multiple gates.
The smallest gate mark is not always the best manufacturing choice. A restrictive entry can increase pressure demand or compromise packing.
Нашите injection molding gate guide explains gate-selection and acceptance considerations.
Design For Release And Handling
Specify suitable draft and consider the effect of texture. Plan ejection support so thin walls do not carry excessive concentrated force.
Check how the part is removed, stacked, and packed. Damage after molding can erase the savings from a faster cycle.
What Machine And Mold Capabilities Matter?
Assess the machine and mold as a matched system using the proposed part, смола, and cavity layout.
ENGEL presents several machine platforms for different thin-wall applications. Това thin-wall molding overview illustrates why application requirements determine the configuration.
Injection Rate, Pressure And Response
Check available volumetric injection rate and pressure under the required operating conditions. Screw diameter affects how screw velocity translates into volumetric flow.
A maximum screw-speed figure alone does not establish filling capability. Acceleration, pressure availability, and the filling-to-packing transition also matter.
Do not assume an all-electric machine is always suitable or a hydraulic machine is always unsuitable. Evaluate the specific injection unit and control response.
ARBURG highlights filling dynamics and precise movements for packaging applications in its packaging-machine guidance.
Clamping And Tool Support
Clamping needs depend on projected area, cavity pressure, and cavity layout. No universal tonnage factor applies to every thin-wall part.
Review mold rigidity and support around slender cores. Deflection during filling can create uneven wall thickness even when the nominal CAD is uniform.
Choose tool materials and heat treatment for wear, смола, геометрия, and intended life. A particular steel grade is not mandatory for every application.
Обезвъздушаване, Runners And Cooling
Provide effective gas escape at relevant end-of-fill regions. Vent dimensions need resin-specific review; excessive clearance can create flash.
Select the runner system using filling, поддръжка, material usage, и икономика. Hot runners are useful in many applications but are not universal requirements.
Cooling must address local temperature balance as well as speed. Conformal channels may help difficult geometry, but conventional channels can suit many tools.
How Should You Develop And Validate The Process?
Validate a repeatable process that delivers acceptable parts, rather than demonstrating one successful shot.
Begin with material preparation and confirmed mold conditions. Review filling, packing, охлаждане, and ejection as connected stages.
A controlled short-shot study can help reveal the filling sequence where appropriate. Compare cavity balance and the locations of hesitation or trapped air.
Evaluate packing before the feeding path seals. Increasing hold time after conventional gate freeze-off cannot add material through that gate.
Confirm ejection readiness and handling stability. A complete-looking part can still distort or fail its functional requirements.
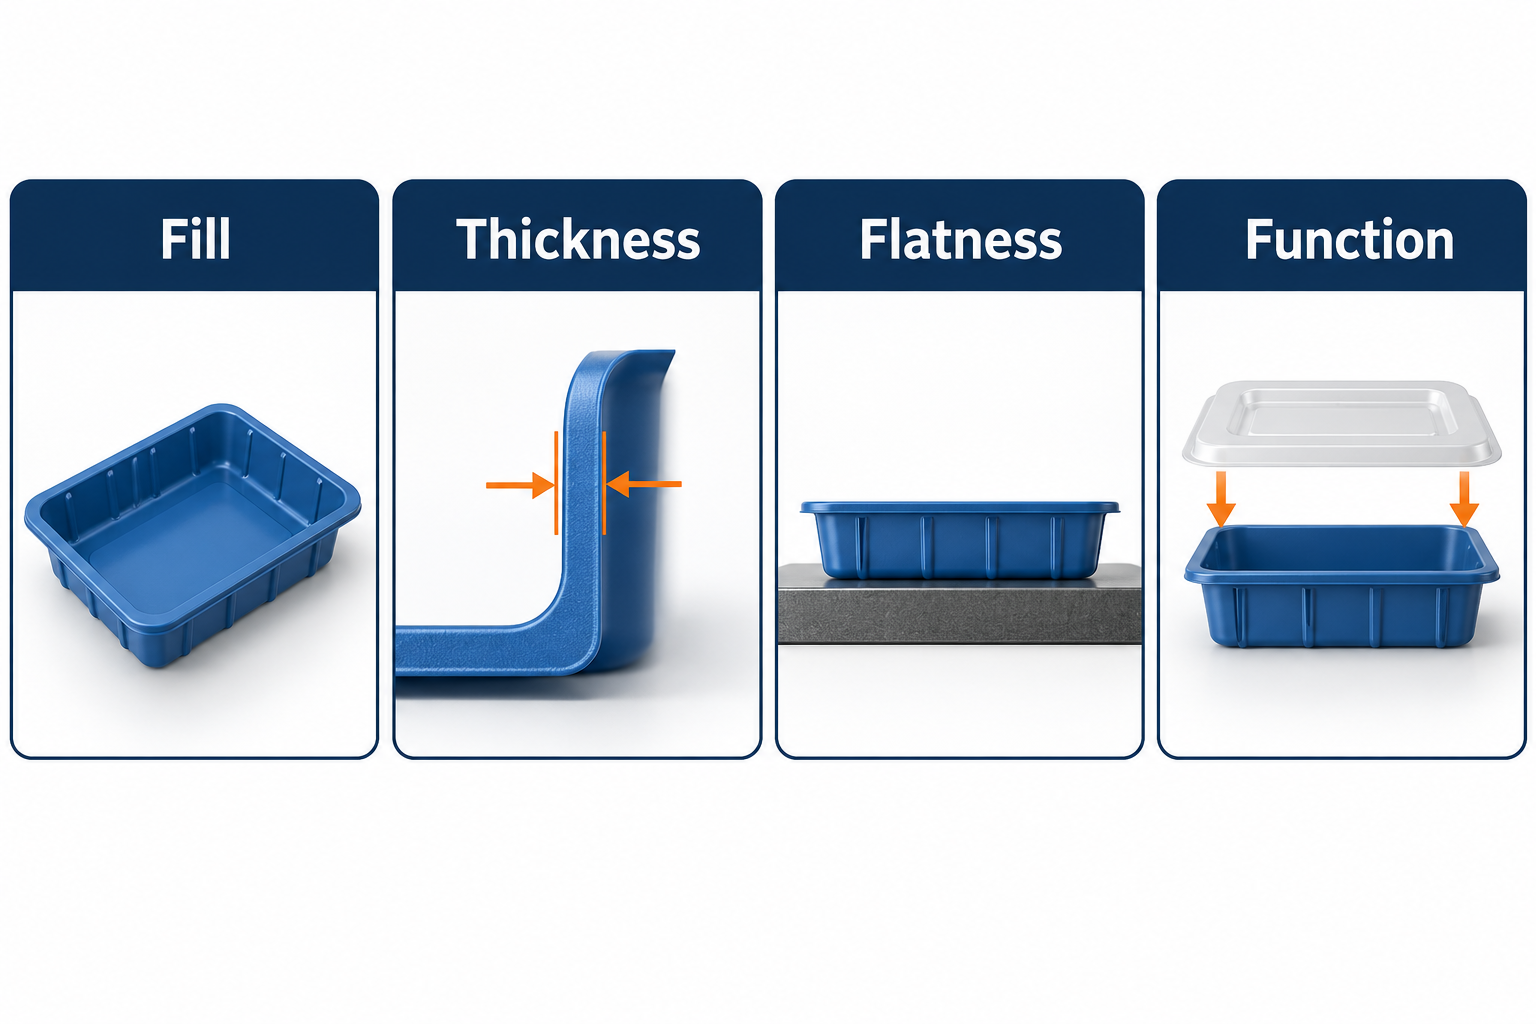
Figure 3. Verify filling, wall distribution, размери, и функция. Conceptual checks, not inspection results.
| Validation Area | Evidence To Request |
| Complete filling | Consistent edge and feature formation across cavities |
| Wall distribution | Measurements at specified locations, including critical minima |
| Dimensions and flatness | Results using agreed conditioning, датата, and support |
| Външен вид | Gate marks, заваръчни линии, Марки за потоци, and approved surface criteria |
| функция | Relevant assembly, drop, stacking, уплътняване, or load testing |
| Process repeatability | Stable-run data and agreed checks following restart |
Use measuring methods that do not distort the thin wall. A heavy contact force can change the value you are trying to measure.
Part weight is useful process evidence, but it does not prove wall distribution or dimensional conformity. Keep cavity identity where traceability matters.
Which Defects Are Most Important In Thin-Wall Molding?
Focus on defects that indicate filling limits, local imbalance, or insufficient support during cooling and release.
Кратки снимки
Check delivery consistency, pressure behavior, local restriction, and venting before increasing speed or temperature.
Faster filling may help prevent premature flow restriction, but excessive entry velocity can create other defects. Test a justified profile within material limits.
Flash And Uneven Walls
Inspect shutoffs, tool closure, and deflection. Determine whether the problem appears during filling or packing.
More clamp force is not a substitute for a damaged or inadequately supported mold. Verify wall thickness after any correction.
Изкривяване
Review cooling balance, packing distribution, ориентация, и изтласкване. Thin walls can expose distortion that assembly fixtures temporarily hide.
Measure under agreed conditions and confirm that the part fits without unacceptable forced restraint.
Weld Lines And Burn Marks
Evaluate where flow fronts meet and where gas must escape. Check functional performance where meeting fronts cross loaded or sealing regions.
A visually cleaner line does not automatically mean adequate strength. Burn marks may require vent or filling-sequence changes rather than simply raising temperature.
For a structured diagnostic method, вижте нашите injection molding defect-prevention guide.
When Does Thin Wall Injection Molding Reduce Cost?
Thin walls reduce cost when material and production savings outweigh added tooling, процес, проверка, and handling demands.
Lower part mass can reduce resin consumption. Shorter cooling may improve output, but thick features and machine movements can still limit the cycle.
Do not equate a percentage reduction in thickness with the same reduction in total cost. Инструментална екипировка, труд, скрап, and secondary operations remain relevant.
Compare proposals using the same resin, acceptance criteria, cavity count assumptions, and order quantities. Include annual demand and program life.
Ask for the estimated cycle basis and identify what trials must confirm. A fast cycle producing unacceptable parts is not a cost advantage.
Нашите injection molding RFQ guide helps separate tooling, recurring production, and delivery costs.
When Should You Consider Another Approach?
Consider alternatives when the required thin section creates unacceptable filling risk, poor service performance, or uneconomic investment.
A modest geometry change may improve feasibility more effectively than purchasing greater machine capability. Compare gate placement, thickness transitions, and part segmentation where appropriate.
For selected broad, thin components, injection-compression molding can be worth evaluating. It uses a controlled compression movement during the molding sequence.
This requires compatible equipment and tooling; it is not a setting added to every conventional process. Вижте ENGEL’s injection-compression explanation.
For suitable open packaging shapes, thermoforming may also deserve comparison. For early development or low quantities, evaluate a prototype route first.
Изберете въз основа на геометрията, допустими отклонения, материал, функция, and realistic demand. Avoid making minimum wall thickness the only success criterion.
What Should You Send For A Thin-Wall Feasibility Review?
Provide the complete design and acceptance requirements so the supplier can evaluate a realistic production concept.
Include CAD, чертежи, nominal and minimum walls, resin grade, повърхностни изисквания, and critical dimensions. Identify gate restrictions and the mating components.
State relevant impact, скованост, уплътняване, околната среда, and appearance requirements. Add order quantities, годишен обем, program life, and target delivery milestones.
TOPS lists plastic injection molding services. Confirm thin-wall feasibility, инструментална екипировка, equipment suitability, and inspection scope for your specific design.
Request A Thin-Wall Part Review with your CAD, resin requirements, wall targets, annual demand, and acceptance criteria.
често задавани въпроси
These answers address common assumptions before you approve a thin-wall design or production quotation.
What Is The Minimum Wall Thickness For Injection Molding?
There is no universal minimum. Resin, flow distance, геометрия, gate arrangement, инструментална екипировка, and equipment determine feasibility. Confirm the proposed wall through analysis and representative trials.
Is A High L/t Ratio Enough To Reject A Design?
не. It signals a demanding flow path but does not include every relevant factor. Use grade-specific analysis and an equipment review.
Does Thin Wall Molding Always Require A Hot Runner?
не. Runner selection depends on filling, разход на материал, gate requirements, и икономика. Compare feasible configurations rather than treating one system as mandatory.
Is The Highest Injection Speed Always Best?
не. The required profile must fill the part while controlling pressure, срязване, trapped gas, and gate behavior. Maximum speed alone is not the objective.
Can Thin-Wall Parts Have Tight Tolerances?
Some features can, but capability depends on geometry, смола, conditioning, and measurement. Ask for confirmation of each critical requirement rather than a blanket tolerance promise.
Does A Thinner Wall Always Mean A Shorter Cycle?
не. Cooling may improve, but local thick sections, plasticizing, mold movements, and handling may still control the cycle.
Заключение
Thin wall injection molding works when geometry, смола, инструментална екипировка, and machine response support the same production target. Evaluate flow distance alongside thickness, then validate wall distribution and function. Compare cost per accepted part before reducing walls further or committing to production tooling.


