

Anodizing tolerances matter whenever your aluminum parts must fit together after finishing. A shaft can grow, while a coated bore can shrink. You need agreed coating allowances, clear drawing notes, and inspection of the finished features. This guide explains how to plan those decisions before machining starts.
How Anodizing Changes Part Dimensions
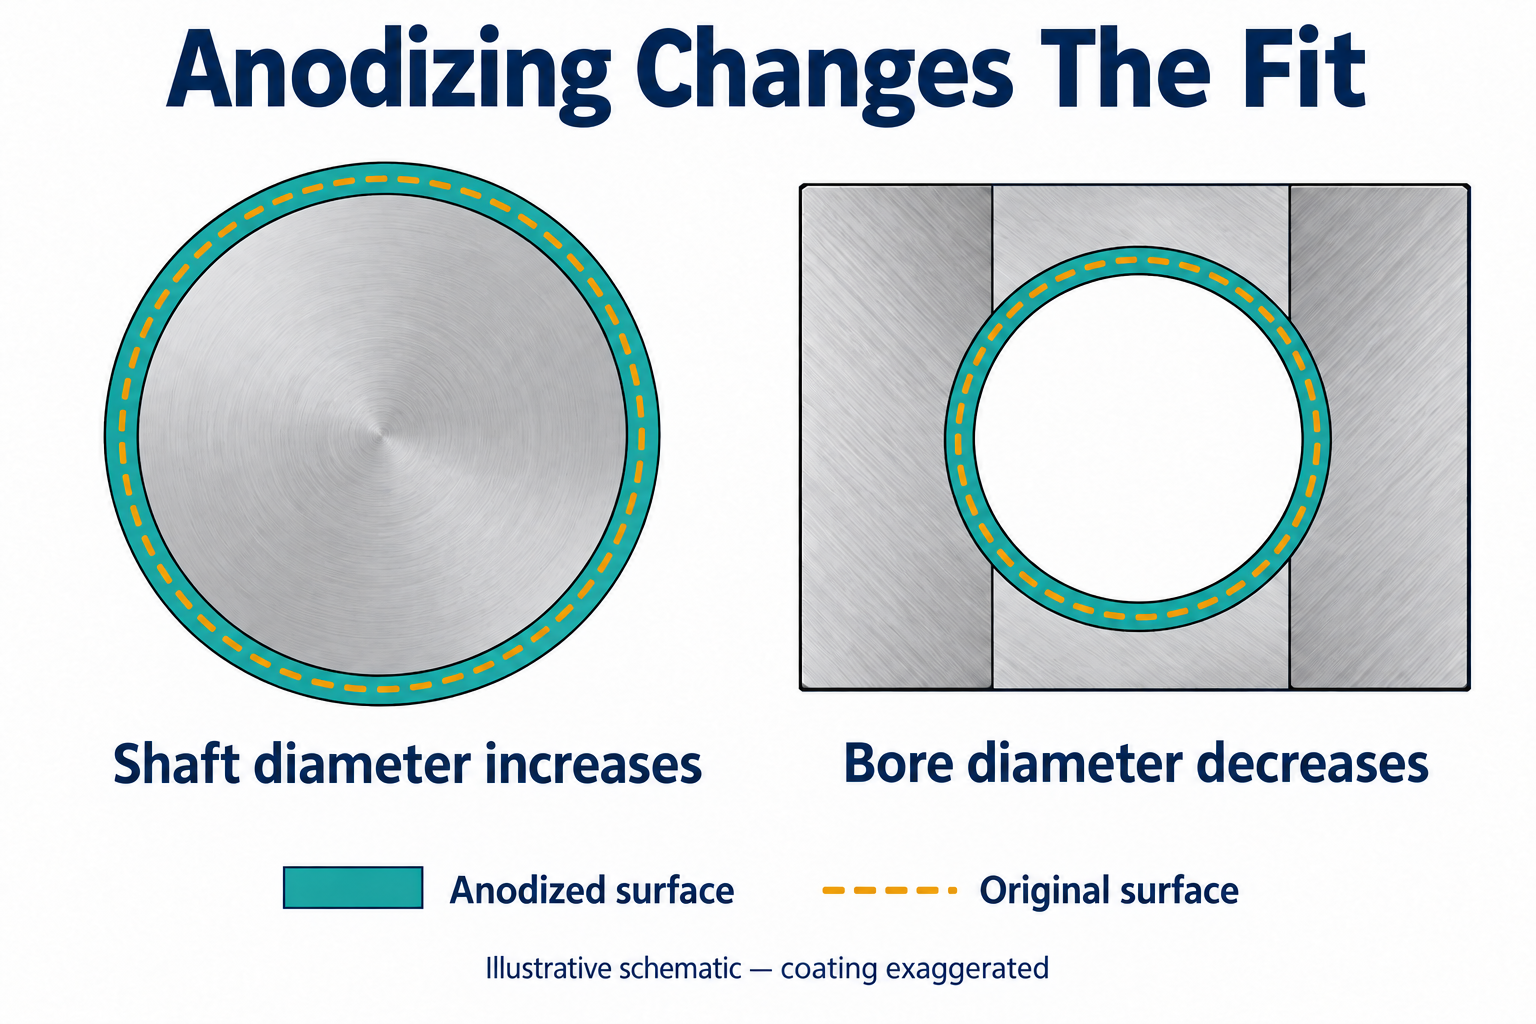
Anodizing converts aluminum into oxide, so coating thickness and outward growth are different measurements.
For hard anodizing, NASA describes a typical split: approximately half penetrates the original surface, while half grows outward. Internal coating thickness can differ from external thickness, particularly in narrow or deep holes. Geometry and bath conditions affect the result. Treat the half-thickness relationship as an estimate, rather than a guaranteed allowance. Voir NASA PRC-5006 Rev. D, Sections 3.1–3.2.
You should distinguish three quantities when discussing a critical feature:
- Coating thickness: the total oxide layer.
- Surface growth: movement beyond the original metal surface.
- Finished dimension: the measurable size after the specified finishing operations.
Pretreatment also matters. Chemical etching can remove aluminum before anodizing. Ask your finisher whether its allowance includes that removal. Le Aluminum Anodizers Council FAQ notes that other line operations affect dimensional changes.
How To Calculate A Preliminary Anodizing Allowance
You can estimate size changes by counting the coated surfaces that affect each dimension.
Let g represent outward growth per surface, measured from the surface immediately before anodizing. Assuming equal growth on opposing surfaces:
| Fonctionnalité | Estimated Finished Size | Practical Effect |
|---|---|---|
| External shaft diameter | Pre-anodize diameter + 2g | A mating fit becomes tighter |
| Internal bore diameter | Pre-anodize diameter − 2g | Available clearance decreases |
| Plate thickness, both faces coated | Pre-anodize thickness + 2g | The thickness stack increases |
| Slot width, both walls coated | Pre-anodize width − 2g | The slot becomes narrower |
These equations describe simple geometry. They exclude pretreatment removal and unequal coating growth.
A Worked Example With Explicit Assumptions
Suppose your finisher confirms an estimated growth of 0.010 mm per coated surface.
- UN 10.000 mm pre-anodize shaft would finish near 10.020 mm.
- UN 10.050 mm pre-anodize bore would finish near 10.030 mm.
- The estimated diametral clearance would decrease from 0.050 mm à 0.010 mm.
This is illustrative arithmetic, not a recommended coating specification or production tolerance. Both parts contribute to the clearance change.
For acceptance planning, calculate minimum clearance using the smallest finished bore and largest finished shaft. Use agreed process limits, not nominal growth alone. Check maximum clearance separately if looseness affects performance.
Which Features Need Special Review?
You should prioritize features whose fit, contact, or function changes when their surfaces are coated.
| Fonctionnalité | Question To Resolve | Possible Drawing Decision |
|---|---|---|
| Bearing seats and locating bores | Must the contact surface retain its coating? | Agree an allowance, masking, or approved final sizing |
| Sliding shafts and slots | What finished clearance and surface condition are required? | Specify final limits and functional checks |
| Sujets | Must threads be coated, and how will they be gauged? | Define masking or a qualified thread allowance |
| Electrical contact pads | Where must conductive contact remain available? | Identify the permitted finish and masked boundaries |
| Datum and mounting faces | Which surface establishes the final measurement reference? | State the required finished condition |
Do not apply a plain-diameter allowance directly to a thread’s pitch diameter. Thread geometry requires a separate review. NASA’s specification discourages hard anodizing on threads and identifies masking or final sizing as options for difficult holes.
When Should You Mask Instead Of Compensating?
Masking is worth considering when a critical surface does not need anodizing and coating variation threatens its function.
Choose the approach based on what the surface must do:
- Compensate before coating when you need the anodized surface and can validate the finished limits.
- Mask the feature when coating is unnecessary there and the exposed surface has an approved protection plan.
- Finish-machine afterward only when removing the coating is acceptable and remaining protection is addressed.
Masking creates additional boundaries to control. Identify where coating may stop, and keep transitions away from critical contact zones where possible.
Hard anodizing is primarily selected for wear resistance or microhardness. Its quality criteria also include final dimensional tolerances. Compare those requirements before choosing it solely for appearance. Voir QUALANOD’s hard anodizing guidance.
For a broader finish comparison, read our guide to anodizing types.
What Should Your Drawing Specify?
Your drawing should define the required finish and clearly identify when each critical dimension must comply.
A color instruction alone cannot communicate the complete acceptance requirement. Inclure:
- The applicable finishing specification and required revision.
- The coating type, class where applicable, couleur, and sealing requirement.
- The required coating thickness and permitted variation.
- Finished dimensional limits for critical features.
- Masked surfaces, boundaries, and permitted rack-contact locations.
- Surface texture and inspection requirements where function depends on them.
Use separate pre-finish and final requirements when both need control. Keep the drawing and CAD model consistent.
Par exemple, add a feature-specific instruction such as: “Bore diameter limits apply after anodizing.” That sentence clarifies timing. You must still supply the actual limits and complete finish specification.
How Should Finished Parts Be Inspected?
You should verify critical dimensions after all specified finishing operations, using an agreed inspection plan.
Before ordering, identify the features that need recorded results. Agree the measurement method, sampling requirements, and acceptance criteria with your supplier.
A useful control sequence is:
- Review the drawing and identify coating-sensitive features.
- Agree machining allowances and finishing requirements.
- Record critical dimensions before finishing when process comparison is needed.
- Complete anodizing and any approved secondary operations.
- Inspect final dimensions, specified coating characteristics, and relevant assembly functions.
A coating-thickness result does not replace a finished bore measurement. De même, a successful trial assembly does not verify every drawing requirement.
For recurring orders, retain approved first-article results and the agreed process conditions. Review changes before altering the alloy, prétraitement, coating specification, or masking plan.
What Drives The Cost Of Anodizing Tolerance Control?
Cost increases when your requirements add handling, validation, inspection, or finishing operations.
Selective masking, difficult rack access, and separate final sizing can add work. Detailed inspection reports also require planning.
You can reduce avoidable cost by identifying functional features early. Keep tighter limits where assembly needs them, and explain the reason. Compare quotations against the same finish condition, masking scope, exigences d'inspection, et quantité commandée.
Planning Your Anodized CNC Parts With TOPS
TOPS offers CNC machining and anodized CNC parts; your drawing determines the requirements that need project-specific confirmation.
Notre Services d'usinage CNC include milling and turning. Vous pouvez également consulter notre anodized CNC machining parts service.
Pour votre projet, request confirmation of the finished tolerances, coating specification, masking scope, and inspection deliverables during quotation. A general machining capability does not establish an achievable tolerance after anodizing.
Questions fréquemment posées
The main questions concern dimensional change, masking, and the condition in which your parts must pass inspection.
Does Anodizing Make Holes Smaller?
Coating growth into a bore reduces its opening. The net change also depends on pretreatment removal and actual internal growth.
Should I Dimension Parts Before Or After Anodizing?
Specify final limits for features that control finished assembly. Add separate pre-finish requirements when manufacturing control also requires them.
Can I Use One Allowance For Every Surface?
Do not assume equal growth throughout a complex part. Ask your finisher to validate allowances at the relevant features.
Can A Tight Bore Be Reamed After Anodizing?
Only if your approved process permits it. Reaming removes coating, so review the resulting surface protection and functional requirements.
What Should I Send For An Anodized Part Quote?
Send your STEP model, dimensioned drawing, alloy and temper, finish specification, quantité, and required delivery date. Highlight critical fits.
Get Your Finished-Part Requirements Reviewed
Define the fit you need after anodizing, then agree the machining and finishing plan around it. Contactez-nous with your model, dessin, finish specification, and quantity to request a project review and quotation.