Hydrogen embrittlement control for plated steel parts starts before surface finishing. You need to connect material condition, in lavorazione, relief treatment, and verification. A good coating appearance or acceptable thread fit cannot establish resistance to delayed cracking.
Identify The Risk Before Plating
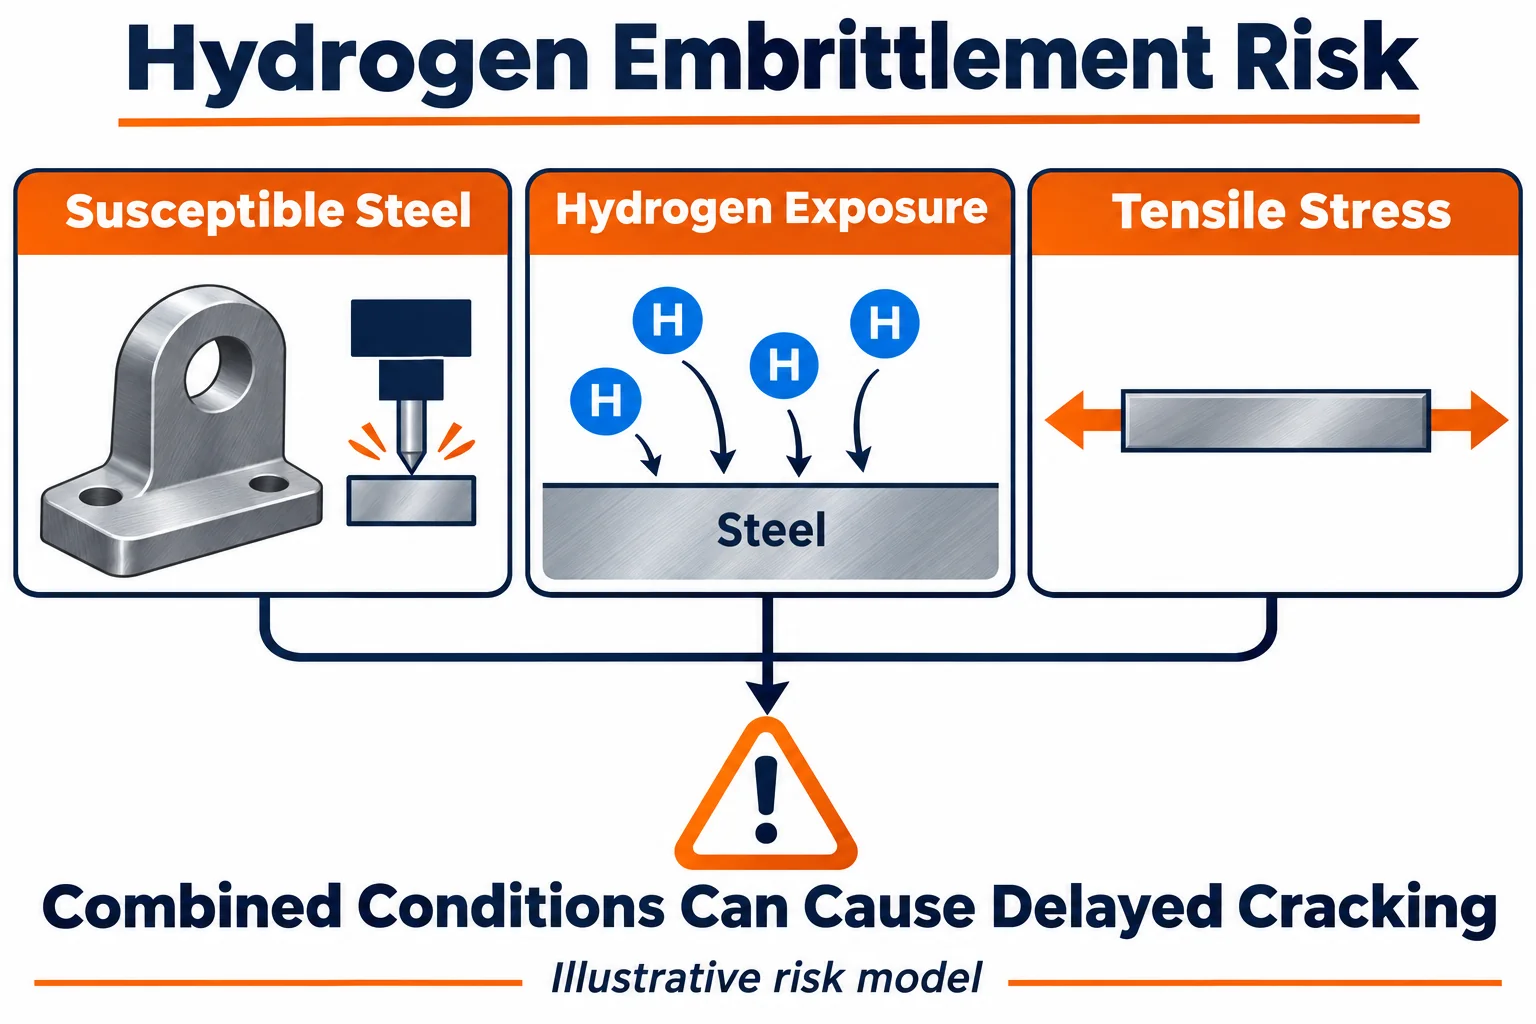
Hydrogen embrittlement risk depends on susceptible material, hydrogen exposure, and tensile stress acting together.
High-strength steel deserves particular review. Specify the actual heat-treated condition, rather than relying only on the alloy name.
Pickling and electroplating can introduce hydrogen. Applied loads and residual stresses can contribute to cracking, which may appear after processing or assembly.
IL AMPP hydrogen embrittlement overview explains the role of hydrogen ingress and tensile stress. Use a materials specialist to assess your component’s susceptibility.
A hardened shaft, loaded pin, or threaded steel component can need different controls. Do not assign one universal hardness threshold to every design and finishing route.
Define The Drawing And Purchase Requirements
Your specification should identify the material condition, sistema di rivestimento, governing documents, and required release evidence.
Resolve these requirements before machining and plating quotes become production commitments.
| Requisito | What You Should Specify |
|---|---|
| Base steel | Material standard, grado, Trattamento termico, strength or hardness requirements |
| Critical features | Loaded sections, discussioni, raggi, condizione della superficie, and dimensional acceptance |
| Fine | Specifica del rivestimento, spessore, conversion treatment, and permitted process route |
| Embrittlement controls | Applicable document revision, required treatments, tempismo, e qualificazione |
| Verification | Test basis, campionamento, criteri di accettazione, record, and release authority |
| Rework | Approval requirements for stripping, sostituzione, and additional treatment |
For dimensional planning, use our thread plating allowance guide. Thread clearance and hydrogen control require separate acceptance evidence.
For new specifications, revisione ISO 24251-1:2025. It addresses high-strength steel components and connects material selection, produzione, Trattamento termico, e rivestimento.
ISO lists ISO 9587:2007 e ISO 9588:2007 as withdrawn predecessors. An existing contract still needs an approved revision decision.
Select documents for your product and process scope. Fasteners and specialized applications can have additional requirements.
Control The Complete Finishing Route
You should control hydrogen exposure throughout preparation and finishing, including any stripping and replating route.
Ask the finisher to identify cleaning, activation, rivestimento, relief treatment, and conversion-coating stages. Record permitted substitutions and approval responsibilities.
Review whether alternative preparation or coating routes reduce exposure while meeting corrosion, adesione, adatto, and service requirements. A process change needs qualification.
Pre-coating stress relief and post-coating hydrogen relief serve different purposes. Specify either operation when required by the governing procedure.
Treat rework as a separate technical decision. Repeating cleaning or plating can change the exposure history and coating condition.
If a supplier proposes an alternative finish, compare its complete preparation route. A different coating name alone does not demonstrate lower risk.
Specify Relief Treatment Without Guessing A Bake Cycle
Relief treatment needs a qualified schedule tied to the steel condition, specifica del rivestimento, and applicable requirements.
ASTM B850-98(2022) provides guidance on post-coating treatment of some steels. It states that heat treatment does not guarantee complete freedom from hydrogen degradation.
Where B850 governs, its stated sequence places treatment after plating and before secondary conversion coating. Resolve sequencing against your approved coating specification.
Ask for the allowed delay, temperature limits, durata, load arrangement, and recorded treatment conditions. Check compatibility with the part’s heat treatment and finish.
Do not copy a temperature and duration from an unrelated drawing. A generic “baked” certificate leaves the actual requirement unclear.
Distinguish Process Verification From Part Inspection
Process verification evaluates the finishing route, while part inspection checks your component’s specified characteristics.
ASTM F519-23 describes mechanical evaluation of plating and coating processes. It supports process qualification and periodic auditing, with defined specimens and acceptance requirements.
Its scope does not rank the relative susceptibility of different steels. Agree applicability and representation with the responsible engineering authority.
| Prova | What It Can Establish | What It Cannot Establish Alone |
|---|---|---|
| Material report | Specified steel identity and reported condition | Acceptability of the later finishing route |
| Treatment record | Recorded processing against an approved procedure | Freedom from every embrittlement failure |
| Process test report | Results for the defined route and test basis | Compliance of every production feature |
| Part inspection | Specified dimensions, aspetto, and coating checks | Absence of delayed hydrogen cracking |
Define how test results connect to the process, fornitore, and production period. A report from another route needs an applicability review.
Compare Supplier Quotes And Release Records
Your quotation should separate machining, finishing controls, verifica, and documentation responsibilities.
Costs depend on material condition, preparation restrictions, treatment scheduling, Test, tracciabilità, and rework limitations. Compare those assumptions before comparing total prices.
Offerte TOP Servizi di lavorazione CNC. Send the complete finish specification with your machining drawing so the proposed manufacturing route can be reviewed together.
Confirm which operations and tests the quotation includes. Identify the finishing provider and the records required before shipment.
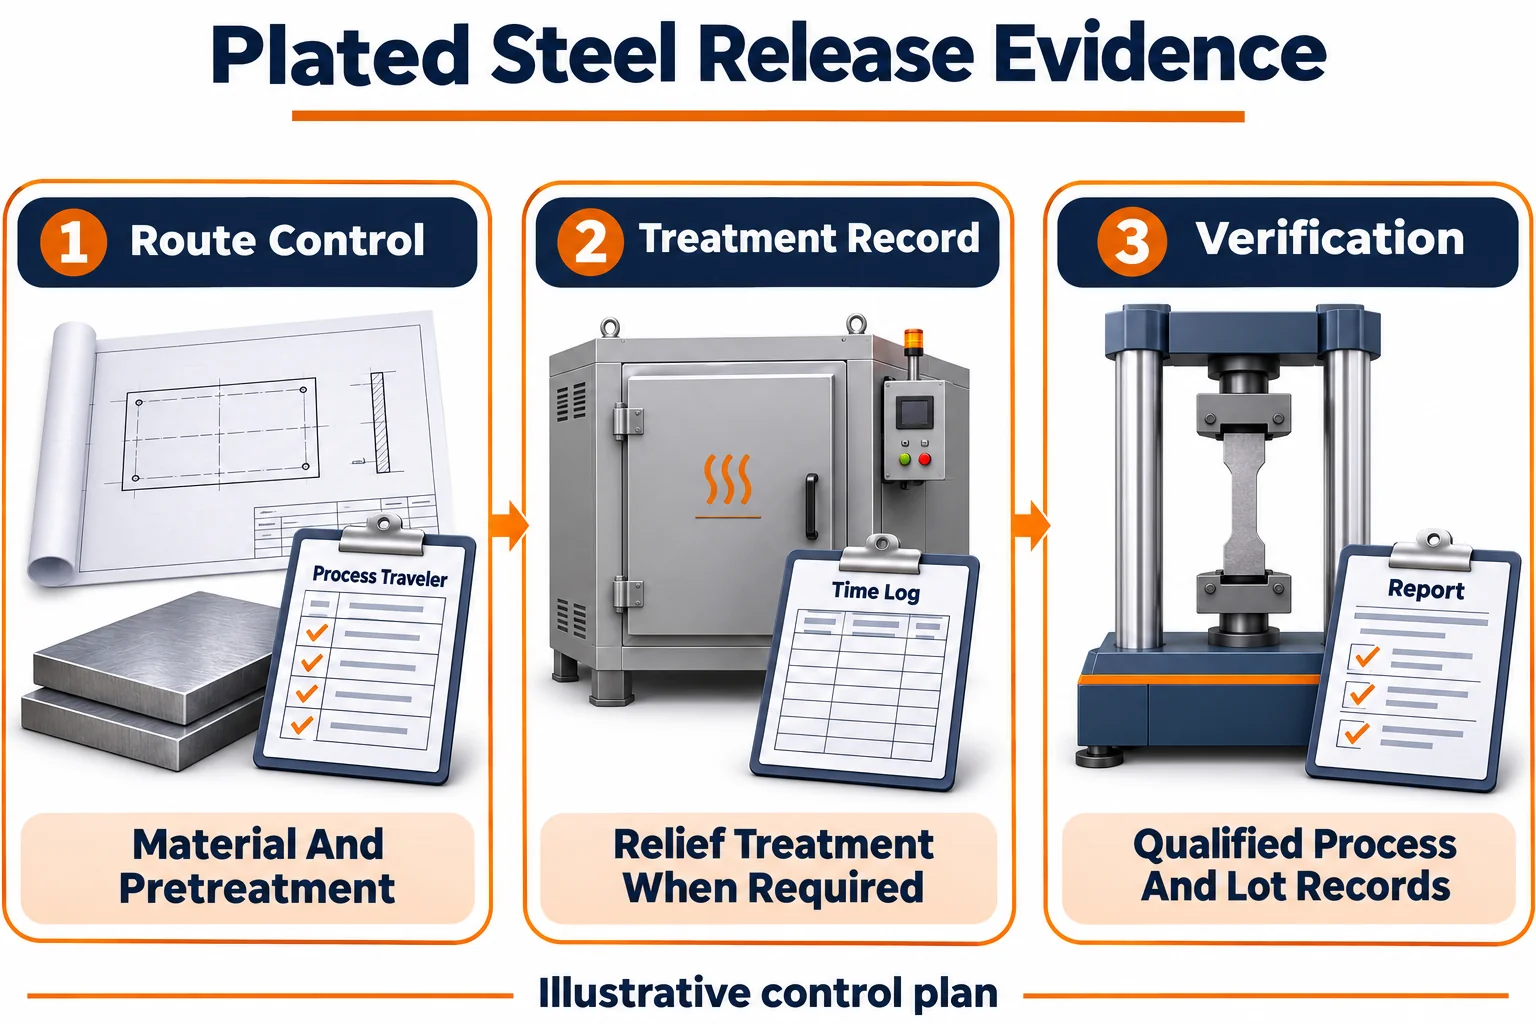
Retain material and heat-treatment records, finishing batch identification, treatment records, required test results, and final inspection evidence.
Domande frequenti
Your purchase agreement should resolve these questions before releasing susceptible steel components for finishing.
Does Every Plated Steel Part Need The Same Controls
NO. Requirements depend on material condition, caricamento, preparation, rivestimento, and the governing product specification.
Can A Visual Inspection Detect All Hydrogen Embrittlement
NO. Acceptable appearance cannot establish freedom from delayed cracking. Use the specified process controls and verification.
Does Relief Baking Guarantee A Safe Part
NO. The approved treatment reduces risk within its applicable scope. It does not replace material selection or process qualification.
Does A Passing Thread Gauge Prove Embrittlement Control
NO. A thread gauge checks fit against its requirements. It does not evaluate delayed cracking resistance.
Can I Use Any F519 Report From The Finisher
NO. Confirm the tested process, conditions, reporting period, acceptance basis, and relevance to your production route.
Is Replating Automatically Acceptable
NO. Obtain approval for stripping, further exposure, dimensional effects, and any required treatment or verification.
Does Manufacturing Control Cover Every Service Environment
NO. Corrosion or other service exposures can introduce hydrogen later. Assess service conditions separately during design review.
What Should I Send For A Quote
Invia il disegno, condizione dell'acciaio, finish specification, quantità, volume annuo, governing revisions, verification requirements, and rework restrictions.
Request A Manufacturing Route Review
Contattaci con il tuo disegno, condizione materiale, coating requirements, and annual volume. Agree the finishing route, verifica, and release records before production approval.