Technical cleanliness for CNC parts means controlling residual particles against your component’s functional requirements. You need more than a washed appearance. Agree the inspected surfaces, extraction procedure, acceptance limits, sampling plan, and delivered packaging before ordering.
Define Technical Cleanliness Around The Part Function
Your cleanliness requirement should protect the surfaces and passages where contamination can affect performance.
Start with the assembly, rather than a generic cleaning instruction. Identify fluid passages, sliding interfaces, sealing faces, or electrical interfaces that need protection. Then define the contamination you need to control.
A hydraulic manifold and an external mounting bracket may need different acceptance criteria. Applying the strictest available test to both can create unnecessary cost. Your design authority should set limits from the actual application.
Separate three requirements in your purchase specification:
Attached burrs and permitted edge condition.
Loose particulate contamination on defined surfaces.
Film, oli, or other residues requiring separate evaluation.
Removing a burr can release particles. Washing can remove loose debris while leaving an attached burr. These operations need different evidence. Nostro cross hole deburring guide explains the edge requirement separately.
Use ISO 16232 Without Inventing A Universal Cleanliness Limit
ISO 16232 provides an inspection framework for automotive component particles, rather than one universal pass limit.
The published ISO 16232:2018 scope covers particulate cleanliness inspection of functionally relevant road-vehicle components. It excludes film contamination, qualitative wipe assessments, and characterization of operating fluids. It also does not prescribe component-specific acceptance limits.
For other industries, agree whether this framework suits your application. Identify the contractual standard and edition explicitly. Do not write only “ISO clean” on the drawing.
You must supply application-specific limits or authorize their development before production approval. If your concern is oil residue, request a suitable separate method. A particle report cannot answer every contamination question.
Write A Cleanliness Specification That Suppliers Can Quote
A useful cleanliness specification connects the tested area, measurable limits, and inspection procedure.
Mark the controlled surfaces on your drawing. State whether internal passages, external faces, or both are included. Altrimenti, suppliers may extract different areas and produce incomparable reports.
| Specification Field | What You Should Define | Why It Changes The Quote |
|---|---|---|
| Controlled area | Marked passages, superfici, and exclusions | Determines access and extraction work |
| Acceptance metrics | Particle sizes, counts, tipi, or mass as applicable | Determines analysis and release decisions |
| Reporting basis | Per component, area, or volume with units | Prevents misleading comparisons |
| Metodo di prova | Agreed extraction and analysis procedure | Defines equipment and laboratory work |
| Sampling and release | Lot definition, sample quantity, tempismo, and failure response | Sets recurring inspection effort |
| Delivered condition | Confezione, chiusure, storage, and receiving checks | Defines protection after cleaning |
Do not copy another product’s particle limits without engineering review. A limit should address your assembly’s sensitivity and achievable manufacturing controls.
Require an explicit response when the supplier cannot meet a field. An unresolved requirement is easier to address before purchase approval.
Qualify Extraction Before Comparing Particle Reports
A particle report is useful only when the extraction procedure represents the surfaces you intend to assess.
HYDAC's technical cleanliness brochure describes extraction approaches including spraying, arrossamento, agitation, and ultrasonics. It also distinguishes gravimetric analysis from microscopic particle characterization. These options provide different information and need application-specific selection.
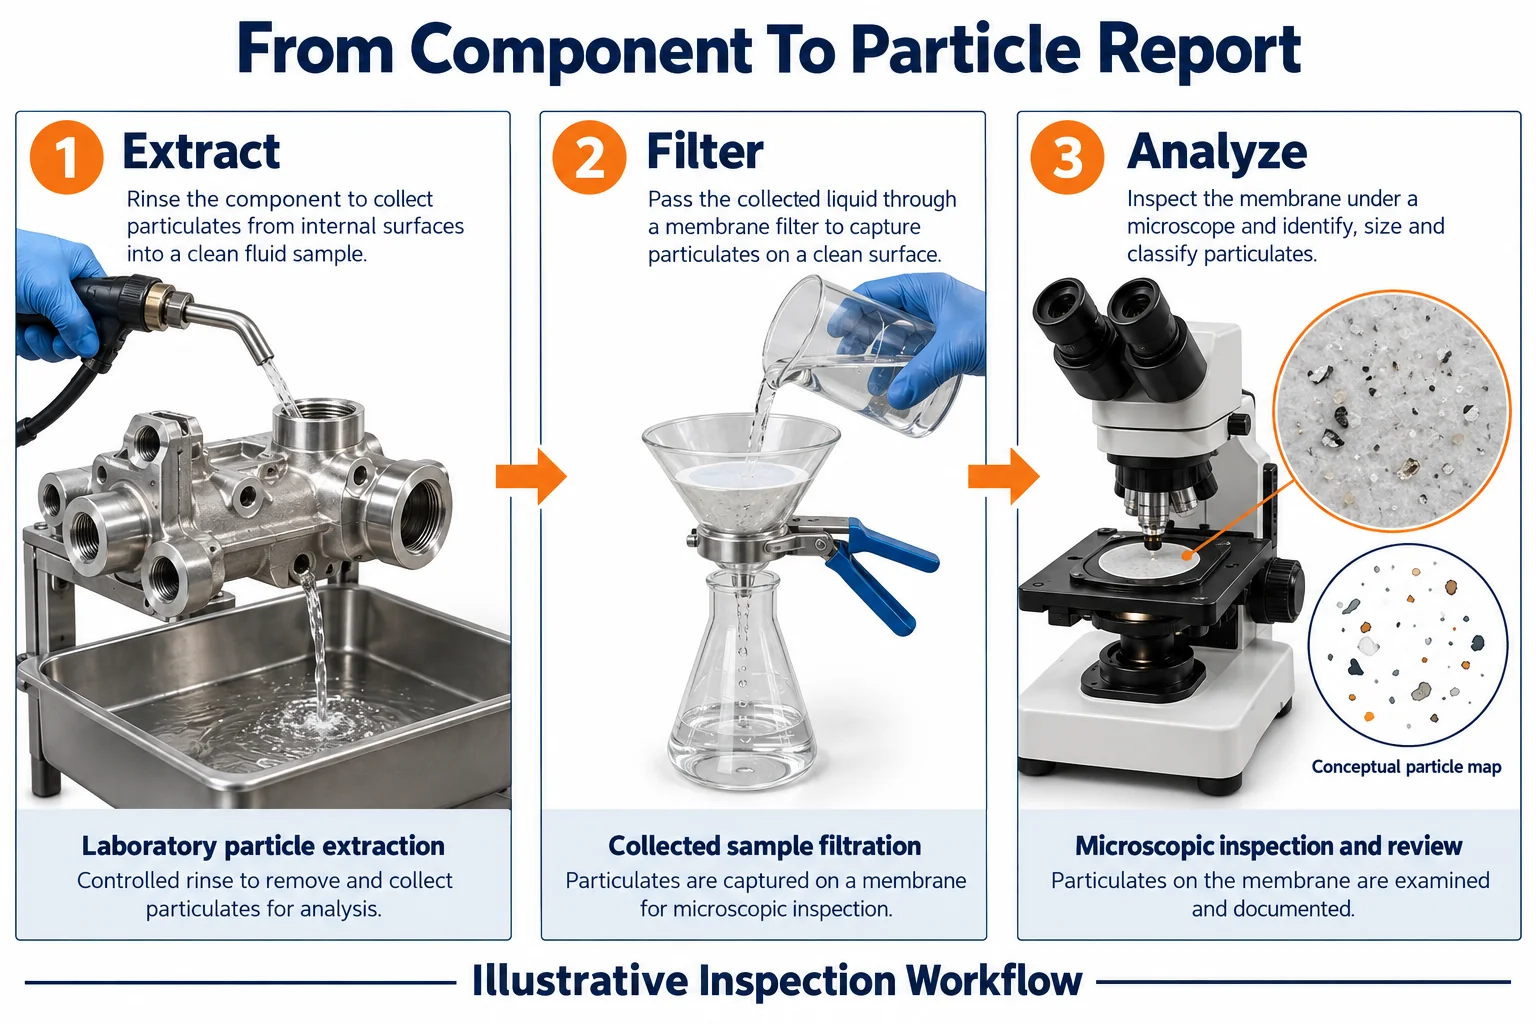
For your part, ask the laboratory how the procedure reaches blind pockets and intersecting passages. Record fluid compatibility, accesso, extraction settings, collection steps, and filtration conditions in the agreed method.
IL ZVEI technical cleanliness guideline explains extraction qualification and equipment blank checks. Ask how your laboratory documents both. The procedure should distinguish contamination from the component from contamination introduced during testing.
Do not change extraction settings between suppliers and assume the results remain directly comparable. Keep the approved procedure revision with the report.
Production washing and laboratory extraction serve different purposes. One prepares the part for delivery. The other collects contamination for measurement. A washing cycle description alone does not demonstrate compliance.
Read Particle Counts With Their Reporting Basis
Particle counts need their size classes, classification rules, and normalization basis to support a purchasing decision.
IL ZEISS explanation of VDA 19.1 reporting describes normalization by component number, wetted area, or wetted volume. You should compare reports using the same agreed basis.
A pooled sample also needs interpretation. An average per component does not identify which individual part carried the particles. Agree whether pooling suits your risk and acceptance plan.
Mass and particle size answer different questions. A low total mass does not identify the largest particle. Particle counts alone do not describe all residue chemistry.
Ask for the information your application needs, without demanding unrelated analyses:
| Report Item | Buyer Review Question |
|---|---|
| Part and lot identity | Does this report represent the shipment? |
| Sample and surface definition | Were the agreed components and areas inspected? |
| Procedure revision | Was the approved method used? |
| Particle results and units | Are results compared against matching limits and bases? |
| Background and deviations | Could testing conditions affect interpretation? |
| Acceptance decision | Who authorized release or corrective action? |
Keep the original results with the release decision. A summary stating only “pass” gives you little information when investigating a later problem.
Preserve Cleanliness Through Packaging And Delivery
Your cleanliness agreement should cover the delivered condition, because handling can reintroduce contamination after washing.
Treat cleaning, ispezione, protezione, and transport as one controlled sequence. Identify operations performed after the final cleaning stage. Include marking, preservation, closure fitting, and packing in that review.
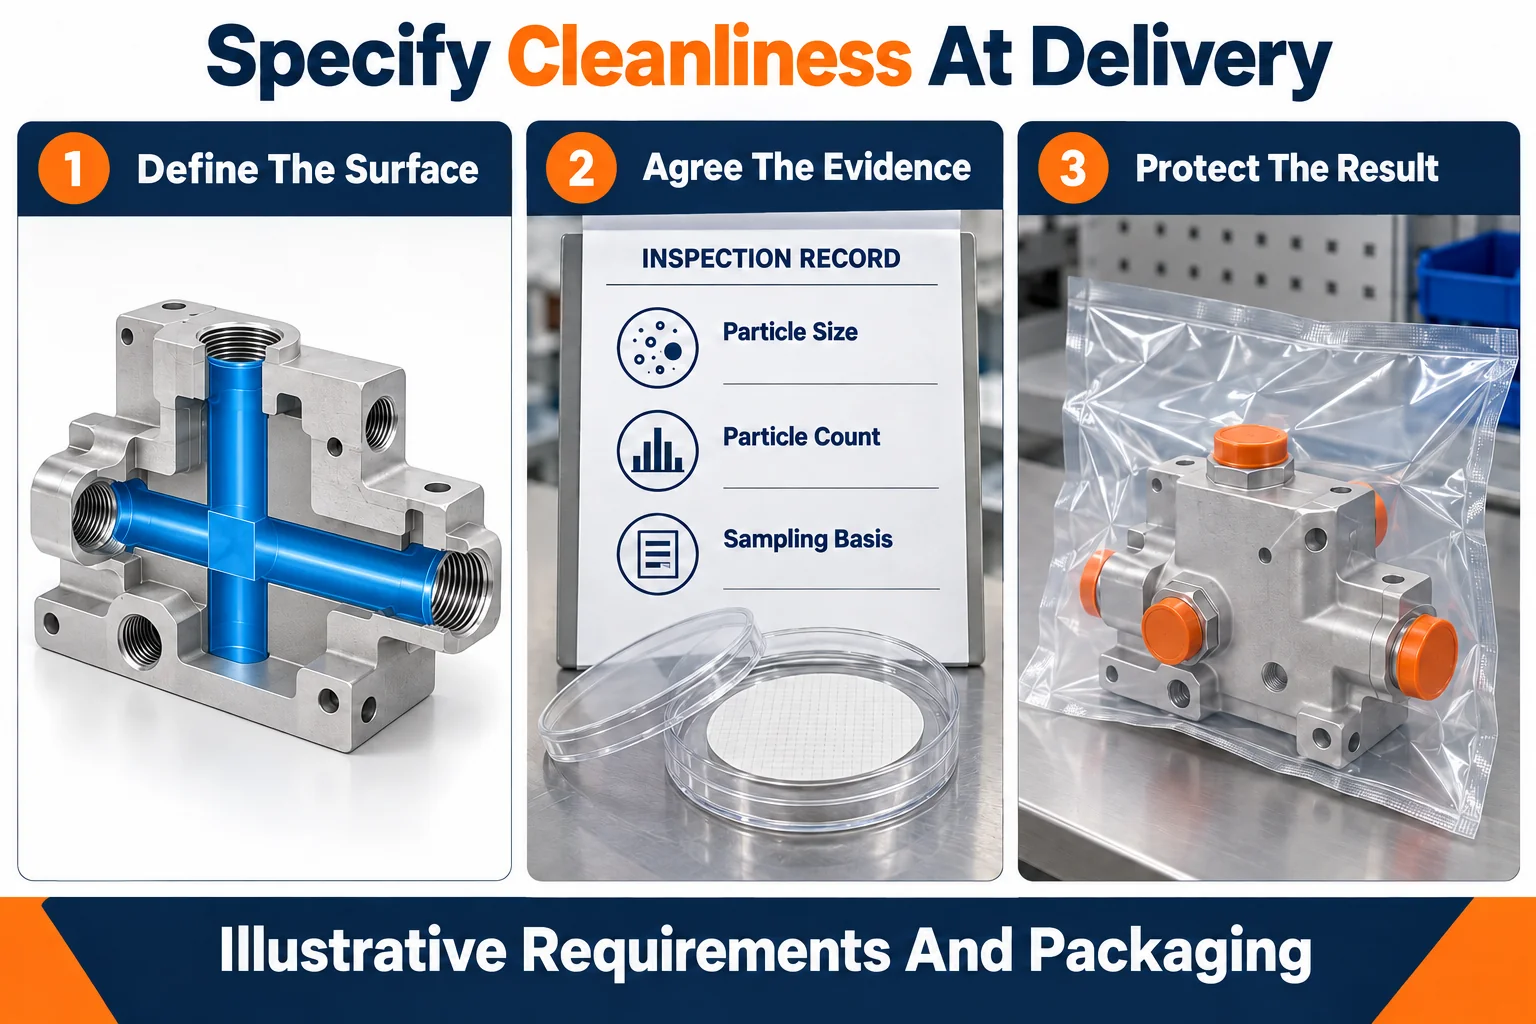
Ask whether protective caps or bags can shed particles into critical features. Agree suitable materials and handling methods. Avoid calling packaging sterile unless a separate validated requirement supports that claim.
Define where acceptance applies. Inspection immediately after washing and inspection after shipment assess different process stages. If receiving inspection matters, agree package opening and sample handling instructions.
For corrosion-sensitive parts, review preservation and cleanliness together. An oil film may protect a surface while conflicting with a separate residue requirement. Resolve that conflict before choosing the shipping condition.
Control Inspection Cost Without Weakening Acceptance
You can control cleanliness cost by specifying the necessary evidence and avoiding ambiguous or excessive requirements.
Cost depends on access, extraction development, analysis complexity, sampling frequency, confezione, and corrective-action workload. Deep passages and restricted access can require additional method development.
Start with a qualification plan for representative production parts. Agree routine monitoring separately. Define when process changes require renewed evaluation, including cleaning chemistry, confezione, or manufacturing sequence changes.
If a sample fails, follow the agreed containment and disposition route. Do not repeatedly wash and retest until one result passes without documenting the investigation. Establish rework authorization and evidence requirements in advance.
Domande frequenti
Your purchasing agreement should resolve the practical questions that a generic “clean parts” note leaves unanswered.
Does A Clean Appearance Prove Technical Cleanliness
NO. Visual assessment cannot substitute for an agreed quantitative particle inspection. Keep cosmetic acceptance and particle acceptance distinct.
Can You Specify ISO 16232 For Every CNC Part
You can propose its framework, but application suitability and contractual scope need agreement. The standard does not supply your component limits.
Is A Milligram Limit Enough
Only when your application supports that metric. If individual particles threaten function, consider size, count, or type requirements as appropriate.
Must Every Part Undergo Laboratory Extraction
Your approved sampling plan determines inspection frequency. Define lot size, sample selection, escalation, and release responsibilities before production begins.
Can A Supplier Guarantee Zero Particles
Avoid an undefined zero-particle requirement. State the measured particle range, inspected surfaces, method capability, and acceptance criteria instead.
Request A CNC Part Cleanliness Review From TOPS
TOPS provides servizi di lavorazione CNC personalizzati. Invia il tuo disegno, materiale, quantità, critical surfaces, cleanliness specification, sampling plan, and packaging requirements. Contattaci to review the manufacturing and verification scope before ordering.