

Powder coating masking for sheet metal protects interfaces that must remain free of powder. Define the protected surfaces, tratamientos restantes, boundary limits, and final acceptance checks before quoting. A color specification alone cannot tell your supplier which threads, almohadillas de contacto, or mating faces need protection.
Identify Every Interface That Must Remain Powder Free
Your masking plan should identify functional interfaces that cannot accept the specified powder coating.
Start with the assembled product. Review threaded hardware, electrical contact locations, close-fitting holes, locating features, and mounting surfaces. Do not mask a surface simply because it appears on a generic checklist.
The design requirement determines whether coating is permitted. Some interfaces need corrosion protection or another treatment even when powder is excluded. Other interfaces may function correctly with coating when the design accommodates it.
Nordson's powder coating guide treats masking as a distinct process step. It describes protecting selected areas before powder application. Your drawing should make those selected areas unambiguous.
| Interface | Pregunta a resolver | Drawing Information |
|---|---|---|
| Internal thread | Must the finished thread remain powder free? | Thread designation, protected depth, and inspection requirement |
| External stud | Which threaded length must remain usable? | Protected length and permitted boundary |
| Electrical contact pad | What finished surface condition supports the connection? | Pad location, tratamiento, and electrical acceptance requirement |
| Mating or locating face | Does coating affect the required assembly condition? | Protected area and finished dimensional requirement |
| Cosmetic surface | Are mask edges or fixture marks visible in service? | Appearance zone and permitted locations |
For the broader finishing process, ver nuestro aluminum powder coating guide. Keep the masking requirement specific to your part and assembly.
Protect Threaded Hardware Before The Finish Process
Thread masking should preserve the required finished fit without relying on unapproved cleanup after coating.
PennEngineering's surface finishing guidance explains that powder coating exceeds the standard thread allowance of self-clinching fasteners. It recommends masking threads and describes plugs for internal threads and caps for external threads.
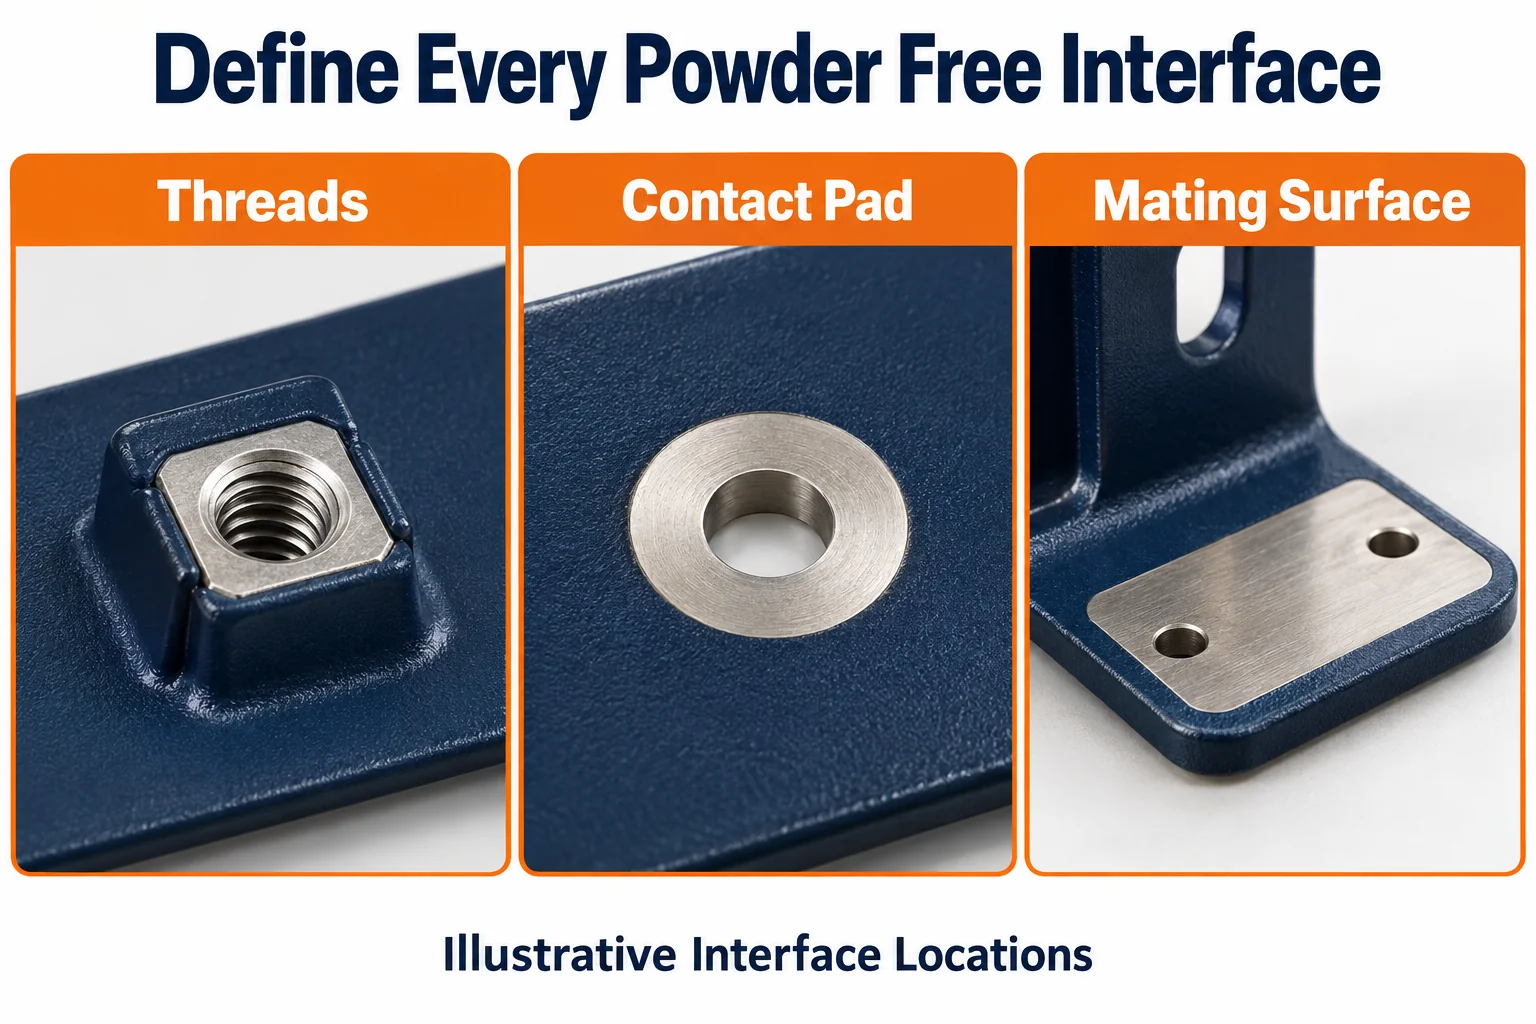
Identify every affected fastener on the assembly drawing. Include blind nuts, through nuts, enfrentamientos, and studs where relevant. A protected entrance does not automatically establish that the entire required thread length is powder free.
Ask how masks are selected, seated, remoto, and checked. Define whether final acceptance requires thread gauging or another agreed functional check. Do not substitute a convenient production screw for a specified inspection method.
If you plan to install hardware after finishing, review that sequence with the hardware manufacturer and fabricator. Installation order can affect access and the finished panel. Nuestro self-clinching nuts guide covers those installation decisions separately.
Define Contact Pads Without Assuming Bare Metal Proves Performance
A powder-free contact pad defines a surface condition, while electrical performance needs its own acceptance requirement.
Por ejemplo, Caplugs' hollow washer plugs mask a hole and a surrounding circular contact area. This shows why protecting only the hole may miss the adjacent surface your connection needs.
Specify the pad location and extent relative to the connection hardware. State whether a conversion treatment, enchapado, or another approved finish must remain. “Bare metal” and “no powder” are different instructions.
Do not infer a qualified bonding connection from appearance alone. Ask the responsible electrical engineer to define the required connection arrangement and verification method. Include assembly hardware, condición de la superficie, and environmental requirements in that review.
Avoid unnecessarily large exposed areas. Your engineering review should balance interface function and corrosion protection. The masking supplier should not have to make that design decision from a photograph.
Put Mask Boundaries And Remaining Treatments On The Drawing
A usable masking drawing defines where powder stops and what surface condition remains inside each protected zone.
Use a dedicated drawing view or clearly identified finish zones. Reference stable features or datums when locating the mask. Avoid relying on an unscaled colored screenshot as the only requirement.
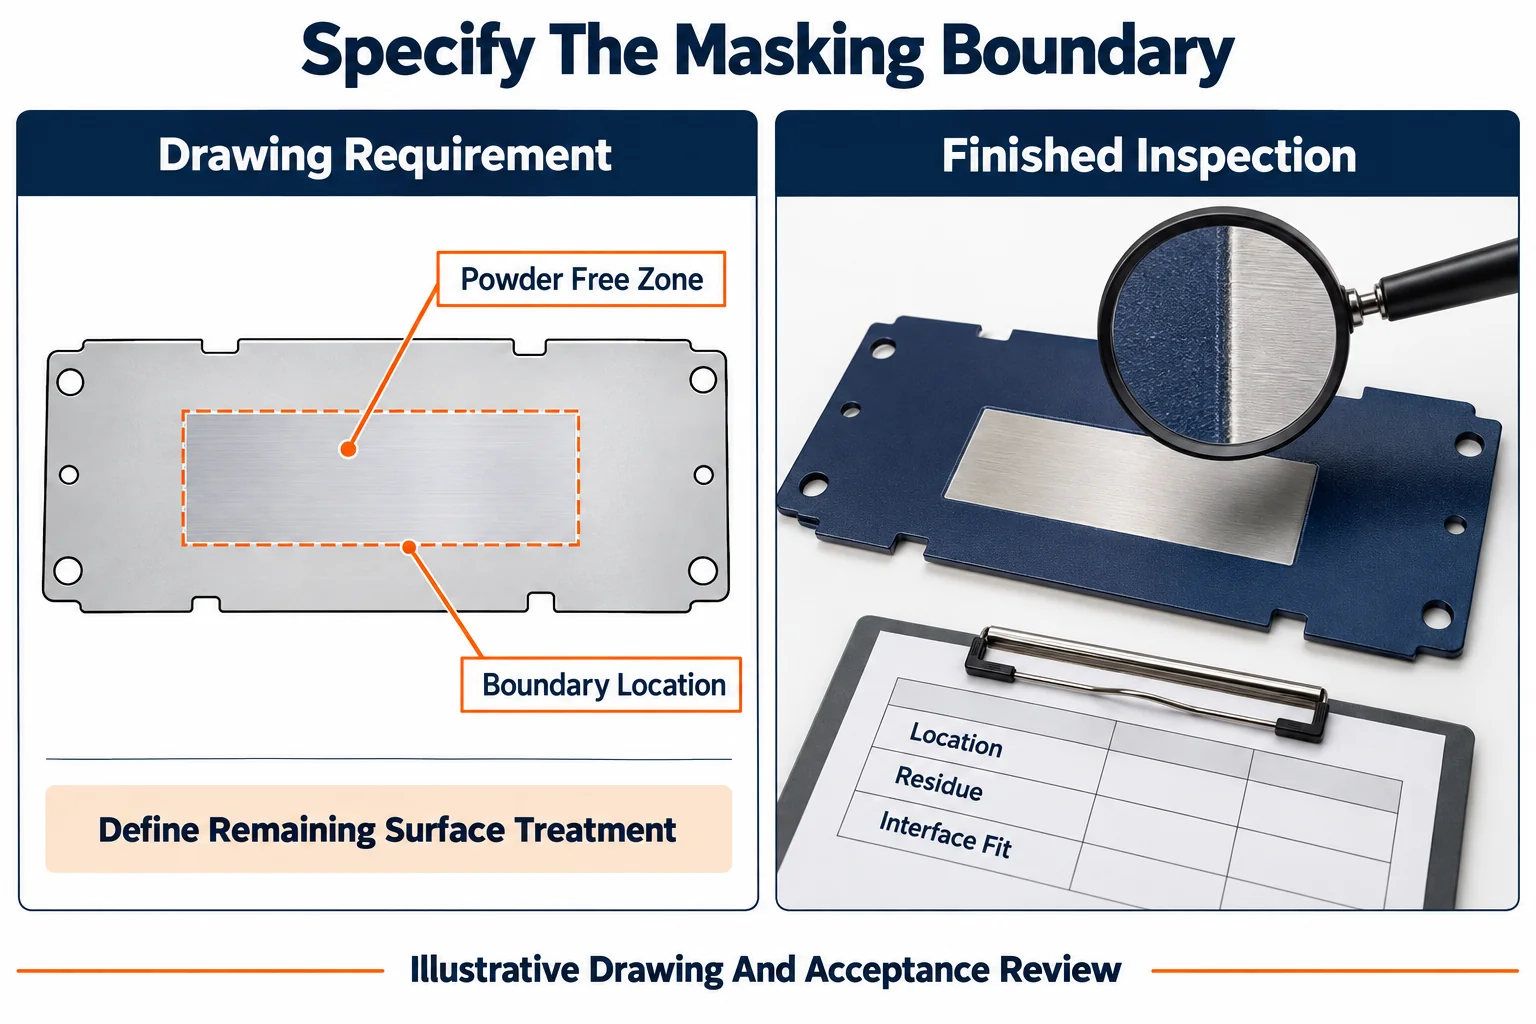
| Requisito | Lo que deberías aceptar |
|---|---|
| Protected zone | Surface identity, location, and extent |
| Layer exclusion | Powder only, or specifically identified additional treatments |
| Boundary acceptance | Permitted transition location and local edge condition |
| Functional condition | Final thread fit, mating geometry, or contact requirement |
| Condición de la superficie | Acceptable residue, tinción, daño, or remaining protection |
| Apariencia | Visible zones and permitted fixture contact marks |
State whether the boundary must remain inside a clearance region or follow a visible cosmetic line. These requirements can lead to different masking methods and inspection effort.
Ask your supplier to flag inaccessible zones or impractical transitions before approval. Complex corners and closely spaced features may need a different mask design. Keep any agreed deviation with the drawing revision.
Select Masks Around The Actual Processing Sequence
Mask selection should match the geometry, exposición química, cure conditions, and required removal quality.
A tape suitable for a flat pad may not protect a deep thread. A plug suitable for one hole may not create the required surrounding contact area. Choose the mask function before selecting a product.
3M's powder coating application profile emphasizes elevated-temperature resistance, defined paint lines, and clean removal. Treat these as selection questions. Follow the chosen product’s current instructions for your actual process.
Request review of the temperature and exposure time, rather than only a headline maximum-temperature rating. Also consider the surface, adhesión, mask geometry, reuse policy, and removal method.
Agree when masks are installed relative to wet pretreatment. PennEngineering warns that caps and plugs applied before wet processing can trap solutions. Review drainage and drying within the proposed sequence.
Do not automatically block pretreatment when you only intend to exclude powder. Identify which layers each masking operation protects. That distinction helps prevent an unintended loss of corrosion protection.
Inspect The Finished Interface After Mask Removal
Final inspection should verify the protected interface after the complete finish and mask-removal sequence.
Check the mask boundary, powder intrusion, adhesive residue, torn mask fragments, and surface damage as applicable. Confirm that required threads and mating surfaces meet their agreed acceptance criteria.
Keep functional and cosmetic checks separate. A neat coating edge does not prove thread fit. An acceptable thread does not prove that a nearby electrical contact pad meets its requirements.
For qualification, review representative finished parts before releasing a larger batch. Agree which checks continue during routine production. Record drawing revision, mask method, resultados de la inspección, and any approved repair.
If coating enters a protected zone, contain the affected parts. Do not chase threads, scrape pads, or remove finishes without an authorized disposition. Rework can change the protected surface and surrounding coating.
Include Masking In The RFQ And Cost Review
A complete RFQ makes masking labor, estampación, inspección, and rework responsibilities visible before production begins.
Send your model, formed-part drawing, material, espesor, hardware list, finish specification, cantidades, and masking view. Identify annual demand where repeat tooling or reusable masks are being considered.
Ask the quotation to distinguish initial mask development from recurring application and removal work. Many small protected zones can demand more handling than one accessible pad. Inspection and cosmetic boundary requirements also affect the scope.
Confirm who approves mask changes and replacement criteria. Establish responsibility for final checks when fabrication and coating involve different suppliers. A low coating price is difficult to compare when those responsibilities remain undefined.
Preguntas frecuentes
Your masking agreement should resolve the practical details that a generic finish note leaves open.
Must Every Hole Be Masked Before Powder Coating
No. Mask only where the design requires powder exclusion. Define the finished hole condition and inspect it accordingly.
Does No Powder Mean Completely Bare Metal
No. Specify whether pretreatment, enchapado, or another approved layer remains. Avoid leaving that distinction to supplier interpretation.
Can You Use Ordinary Tape For Powder Coating
Do not assume suitability. Select a product against the actual process, superficie, geometría, exposición, and removal requirements.
Can Threads Be Cleaned After Coating Instead Of Masked
Only through an approved process. Define any permitted material removal, remaining protection, and final thread acceptance before production.
Does An Exposed Contact Pad Guarantee Electrical Bonding
No. The connection design and agreed electrical verification determine acceptance. Appearance alone cannot establish the required performance.
Request A Sheet Metal Masking Review From TOPS
TOPS ofertas custom sheet metal fabrication. Envía tu dibujo, hardware list, requisitos de acabado, cantidades, and identified powder-free interfaces. Contáctenos to review the fabrication, enmascaramiento, and final inspection scope before ordering.